-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Why Choose Foil Roll for Global Packaging Needs?
In practical packaging work, material choice affects protection, efficiency, and customer trust. Foil Roll remains a strong option for products facing moisture, oxygen, light, or temperature changes. Its reflective surface can help reduce heat exposure during storage and transport. Its compact form also supports high-speed converting and customized package sizes.
The right structure depends on the product. Pharmaceutical applications may require controlled thickness, clean surfaces, and verified barrier performance. Food manufacturers often examine seal strength, pinholes, migration data, and printing quality. Industrial users may prioritize durability, flexibility, and resistance to chemicals. These decisions should follow documented testing, not attractive claims. A qualified supplier should provide technical data, traceability, and consistent batch control.
Global packaging needs also demand careful attention to regional standards and recycling systems. Foil can protect products with very little material, yet its recovery depends on the final package design. Thin foil laminates may perform well but can be difficult to separate. That limitation deserves honest discussion. No material solves every packaging problem. Not by itself.
A reliable selection process compares barrier requirements, forming behavior, sealing conditions, logistics, and total cost. It also considers production waste and the customer’s disposal environment. Experienced teams should test samples under realistic humidity, pressure, and transport conditions. Small defects can become expensive failures. Foil Roll is valuable when its technical strengths match the application, the supplier is accountable, and performance is measured from production line to end use.
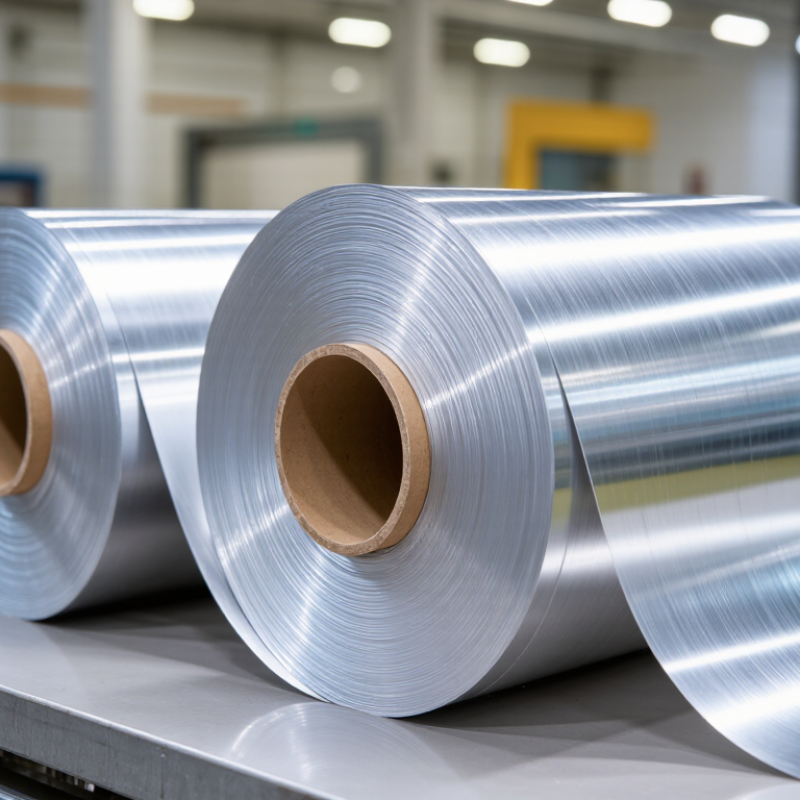
Table of Contents [Hide]
What Foil Roll Is and How It Functions in Packaging
Why Choose Foil Roll for Global Packaging Needs?
What Foil Roll Is and How It Functions in Packaging
Foil roll is a continuous sheet of aluminium supplied in large industrial coils. Converters slit, laminate, print, or form it for different packaging structures. Its main function is barrier protection. The metal blocks light, oxygen, moisture, and many aromas. This helps protect sensitive products during storage and transport.
Thickness matters. A thinner foil can reduce material use, but it may tear during converting or filling. A thicker grade offers better puncture resistance, although it adds weight and cost. In practical packaging trials, weak seals often cause more failures than the foil itself. That detail is easy to overlook. The International Aluminium Institute reports that recycling aluminium uses roughly 5% of the energy required for primary production. However, laminated foil structures can be difficult to separate and recycle. Design decisions should consider the full package, not only the foil layer.
Tips: Specify the required barrier level before selecting thickness. Test rolls under actual humidity, temperature, and filling conditions. Check edge quality, winding tension, and seal compatibility. The FAO estimates that 14% of food is lost between harvest and retail, so reliable barrier packaging can support waste reduction. Still, foil is not automatically the best choice. Engineers should compare protection, recyclability, machine performance, and total material use.