-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

What Is an IML Container Manufacturer?
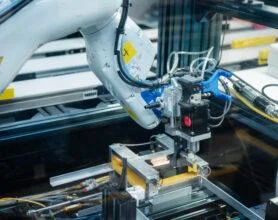
An Iml Container Manufacturer does more than produce plastic containers with attractive graphics. It combines injection molding, label engineering, automation, and quality control within one manufacturing system. During production, a robot places a printed polypropylene label inside an open mold. Molten plastic then fuses with the label, creating a durable, integrated surface. There is no separate labeling line afterward.
According to packaging-process specialist Dr. Marco de Bruin, “In-mold labeling succeeds when the label, resin, mold, and robot work as one process.” This practical observation explains why choosing an IML Container Manufacturer requires more than comparing unit prices. Experienced manufacturers evaluate label adhesion, wall thickness, cycle time, color accuracy, and container performance under real handling conditions. They may inspect a finished tub under bright light, checking for wrinkles, bubbles, or uneven edges. Small defects can damage shelf appeal and increase waste.
A reliable manufacturer should also explain its materials, testing methods, production capacity, and traceability procedures. Food-contact applications demand documented compliance and controlled hygiene practices. Recyclability also deserves careful discussion, because label and container materials must be compatible with local recycling systems. The answer is not always simple. A glossy container may look sustainable, yet its full environmental impact depends on resin choice, decoration, transport, and recovery infrastructure. This article examines what an IML Container Manufacturer actually does, how its process works, and which questions buyers should ask before approving samples. The explanation may not cover every factory variation, but it offers a practical starting point for informed evaluation.
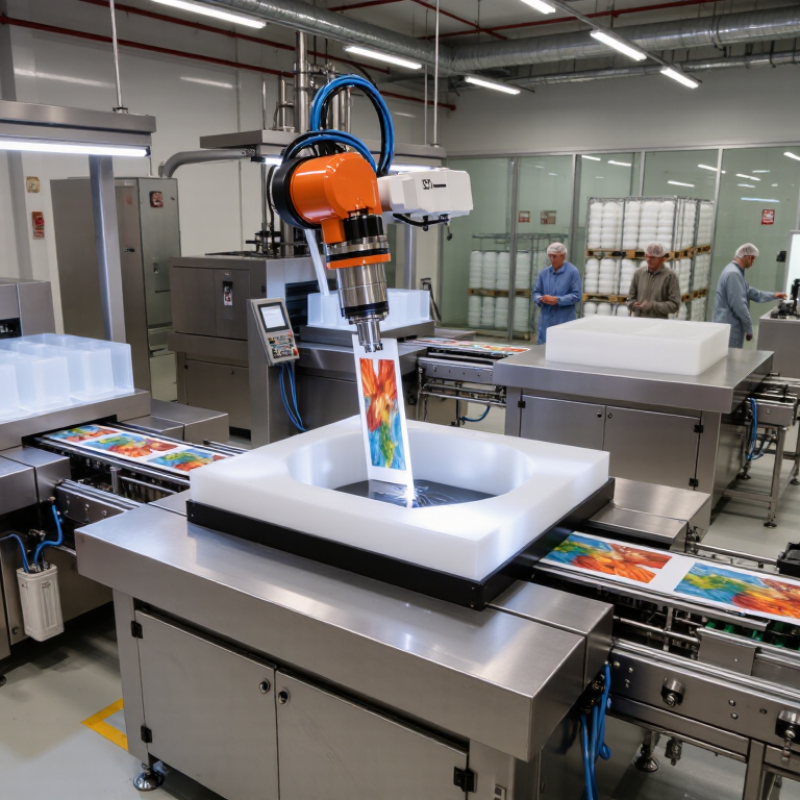
Table of Contents [Hide]
What Is an IML Container Manufacturer? Definition, Role, and Scope
What Is an IML Container Manufacturer? Definition, Role, and Scope
An IML container manufacturer produces containers using in-mold labeling technology. During molding, a printed label is placed inside the mold before plastic is injected. The label becomes part of the container surface. This creates a clean, durable finish without a separate labeling stage.
The manufacturer’s role extends beyond molding. It may support container design, mold development, label specifications, material selection, production testing, and quality control. Engineers must consider label position, wall thickness, cooling behavior, and stacking strength. Small changes can affect appearance and performance. Practical experience matters here. A container may look correct but fail during filling, transport, or repeated handling.
The scope also includes process coordination. A reliable manufacturer checks artwork dimensions, label adhesion, color consistency, and surface defects. It may perform drop tests, compression tests, and dimensional inspections. Food, household, and personal care containers often require carefully controlled materials and documented production records. Requirements vary by application and market, so assumptions can create costly problems.
The process is not flawless. Static electricity, label movement, or uneven cooling may cause visible defects. These issues require investigation, not quick excuses. Manufacturers should explain their testing methods and acknowledge where their process needs improvement. Customers can then judge capability through samples, technical records, and clear communication. Experience is useful, but measurable evidence is stronger.