-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top Spindle Hub Bearing Assembly Manufacturers?
Choosing China’s top Spindle Hub Bearing Assembly manufacturers requires more than comparing prices. Quality depends on materials, machining accuracy, heat treatment, sealing, and final inspection. This guide examines suppliers through those practical factors, rather than relying only on marketing claims or factory size.
Fit comes first. Manufacturers should demonstrate experience with wheel-end systems, spindle tolerances, bearing preload, and demanding operating conditions. Look for clear drawings, traceable material certificates, inspection records, and documented quality procedures. Reliable suppliers can explain their production process from forging or machining to assembly and packing. They should also discuss load ratings, lubrication, corrosion protection, and expected service life in measurable terms.
Details matter. A serious evaluation may include sample testing, dimensional checks, hardness verification, and installation trials. It should also review communication speed, engineering support, minimum order quantities, and replacement availability. Certifications can support credibility, but they do not replace independent verification. That assumption fails.
This article presents a practical framework for identifying capable Chinese manufacturers and comparing their strengths. Some suppliers may excel in custom engineering, while others focus on high-volume production or commercial vehicle applications. Their capabilities can change over time, so buyers should confirm current equipment, standards, and references directly. The strongest decision combines technical evidence, factory experience, transparent communication, and consistent delivery performance. Even a well-prepared shortlist needs review before a long-term purchasing agreement.
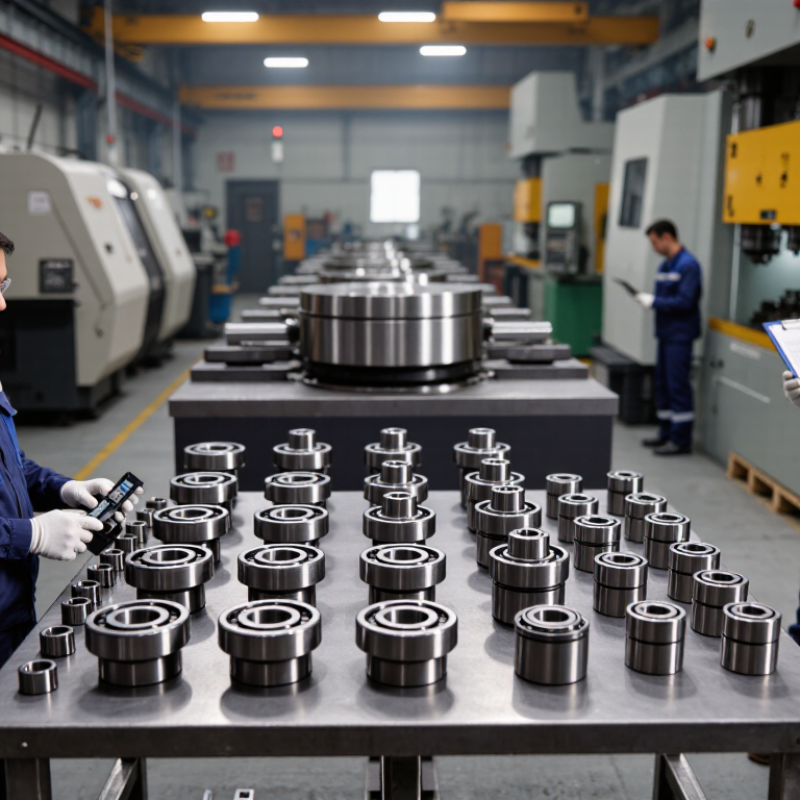
Table of Contents [Hide]
What Is a Spindle Hub Bearing Assembly?
What Is a Spindle Hub Bearing Assembly?
A spindle hub bearing assembly is a precision wheel-end component. It supports the hub, controls wheel rotation, and carries radial and axial loads. The assembly usually combines a bearing, hub flange, seals, and mounting features. Some designs include an integrated speed sensor. This reduces separate installation steps.
During inspection, I look for smooth rotation, correct preload, and even seal seating. A healthy assembly should rotate quietly without grinding or side play. The hub must also align accurately with the spindle and brake components. Small installation errors can create vibration, uneven tire wear, or premature bearing damage. Clean handling matters. Dirt can enter quickly.
Tips: Check the part number, mounting pattern, and sensor connector before installation. Use calibrated tools for fastener torque. Never force the assembly with a hammer. If resistance appears, inspect alignment and corrosion first.
Experienced technicians should also verify the spindle surface. A worn seating area may prevent proper bearing alignment. I have seen new assemblies fail because the mounting face was not cleaned. That mistake is easy to overlook. Temperature, load, road moisture, and maintenance quality affect service life. Manufacturer selection should include material quality, dimensional testing, sealing performance, and traceable inspection records. A low price alone says little about reliability. Even a detailed checklist can miss a hidden spindle defect.