-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

7 Best Solar Cell Cassette Manufacturers?
Choosing among the 7 Best Solar Cell Cassette Manufacturers? requires more than comparing catalog prices. A cassette may look simple, yet it controls wafer positioning, airflow, thermal exposure, and handling stability. Small dimensional errors can create edge contact, uneven coating, or costly cell breakage. Production teams should examine material quality, flatness tolerance, contamination control, automation compatibility, and cleaning procedures. They should also request test data, not rely on polished marketing language.
Dr. Pierre Verlinden, a respected photovoltaic manufacturing specialist, has stated, “A high-efficiency cell is valuable only when it can be manufactured consistently.” That principle fits the Solar Cell Cassette market closely. The best supplier is not always the largest one. It may be the manufacturer that maintains stable tolerances after repeated furnace cycles and provides responsive technical support. Ask for evidence. Inspect sample cassettes under realistic loading conditions. Check whether surfaces remain smooth after handling, especially around slots, corners, and contact points. These details matter on a busy production line.
This comparison considers practical performance, engineering experience, customization, durability, and after-sales reliability. It also recognizes an uncomfortable limitation: supplier data is not always presented in equal formats. Some claims require independent verification. A cassette that performs well in one cell architecture may disappoint in another. Therefore, this guide offers a careful starting point, not an absolute verdict. Manufacturing conditions change. So do priorities.
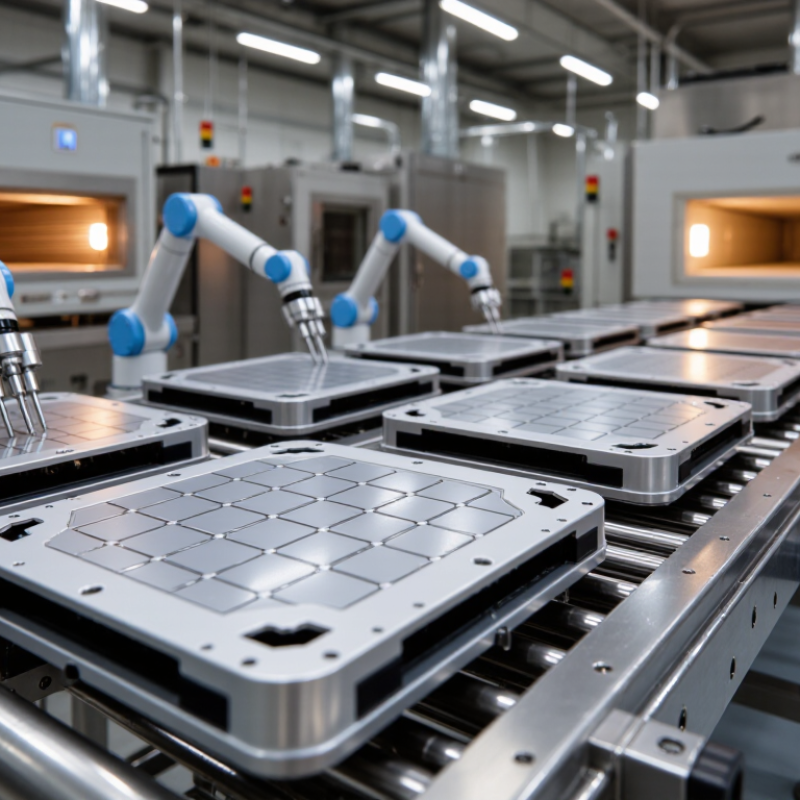
Table of Contents [Hide]
Solar Cell Cassettes Explained: 182 mm, 210 mm, and 25-Wafer Formats
Solar cell cassettes are not simple plastic boxes. They control wafer spacing, edge support, robotic access, and breakage risk. For 182 mm and 210 mm wafers, pocket geometry matters more than appearance. A 210 mm wafer needs greater clearance, while a 182 mm design may allow tighter equipment layouts. Small errors can become costly.
The International Technology Roadmap for Photovoltaic (ITRPV), 2024 edition, expects wafer thickness to decline toward about 120 micrometres by 2034. Thinner wafers demand softer contact points and better control of vibration. The report also shows continued movement toward larger, high-efficiency wafer formats. That trend makes cassette compatibility a production issue, not merely a purchasing detail. Inspect slot pitch, wafer bow clearance, material cleanliness, and robot alignment before selecting a manufacturer.
The 25-wafer cassette remains practical for loading, transport, and process balancing. It limits stack weight and simplifies visual inspection. SEMI wafer-handling guidance emphasizes repeatable dimensions and contamination control, both essential in automated lines. IEA PVPS Trends 2024 reported more than 400 GW of new solar capacity installed globally in 2023, increasing pressure on stable, scalable manufacturing. Yet larger wafers can expose weak cassette designs quickly. A useful factory test includes repeated loading, thermal cycling, and edge-chip inspection. The imperfect part is often overlooked: a cassette may fit mechanically but still fail after months of cleaning and vibration.