-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Top Fusion Welding Machine Manufacturers How to Choose?
Choosing among top Fusion Welding Machine manufacturers requires more than comparing catalogue prices. The right supplier depends on material, pipe diameter, joint design, production volume, and local service capacity. That sounds obvious. It is often missed.
Market data confirms why this decision deserves discipline. MarketsandMarkets estimates the global welding equipment market will grow from about USD 8.3 billion in 2023 to USD 10.4 billion by 2028. Grand View Research also reports steady expansion, although its market boundary differs. These figures are useful signals, not purchasing instructions. Reports may classify robotic systems, consumables, and plastic pipe equipment differently. A careful buyer should question every headline number.
For thermoplastic pipe work, ISO 21307 and ASTM F2620 provide practical benchmarks for butt-fusion procedures. A credible manufacturer should explain heating-plate temperature stability, pressure control, alignment accuracy, data logging, and calibration. Ask for weld records from a machine operating on your actual pipe material. Request service response times, spare-parts availability, operator training, and independent test evidence. A polished brochure is not proof. Neither is the lowest quotation.
The strongest comparison combines factory capability with field experience. Visit a production site when possible. Inspect clamps, hydraulic fittings, electrical protection, and the control interface. Then compare warranty terms and lifecycle costs. Some manufacturers excel in heavy infrastructure, while others suit workshops or portable repairs. There is no universal winner. Even this method has limits, because market growth cannot predict your soil conditions, crew skill, or project delays. The final choice should be documented, technically justified, and tested before full deployment.
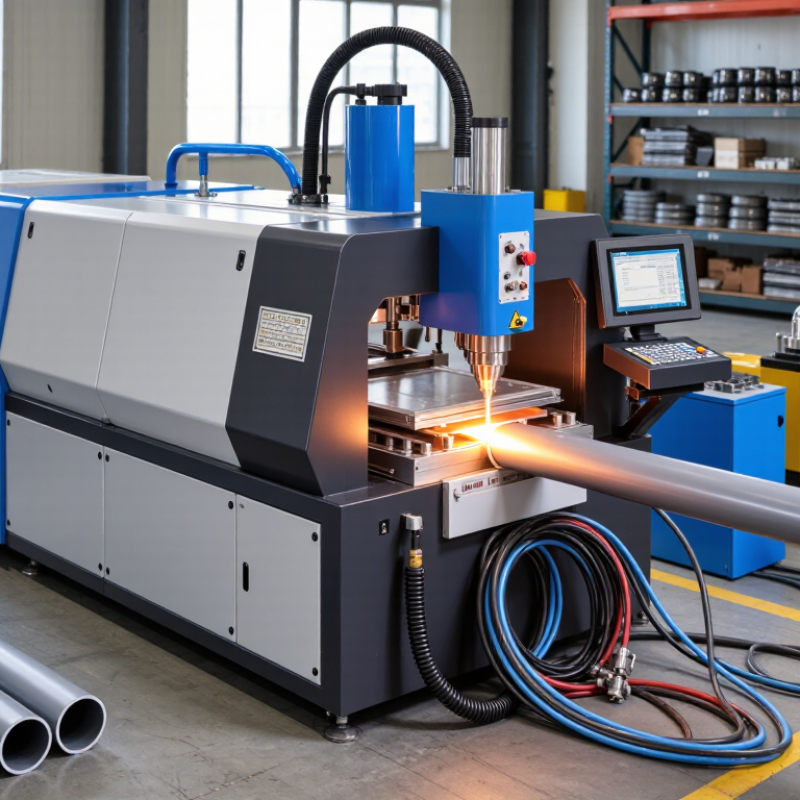
Table of Contents [Hide]
What Is a Fusion Welding Machine and How Does It Work?
A fusion welding machine joins thermoplastic pipes by heating their matching surfaces until they become soft. The operator clamps each pipe in a rigid frame. A facing tool then removes uneven edges and creates clean, parallel ends. A heated plate touches both surfaces at a controlled temperature. After heating, the plate moves away quickly. The softened ends meet under measured pressure and cool into one continuous joint. Some equipment uses hydraulic clamps, while electrofusion machines energize wires molded inside a fitting. The principle remains simple: heat, align, press, and cool.
The Plastic Pipe Institute’s Handbook of Polyethylene Pipe identifies alignment, temperature, pressure, and cooling time as critical quality factors. A 2024 MarketsandMarkets report also links fusion equipment demand with expanding water, gas, and industrial pipe infrastructure. These figures show market momentum, but they do not guarantee a sound weld. Field conditions still matter. Dust on a pipe face can become a hidden leak path. Wind can cool the joint too quickly. I have seen operators trust automatic settings without checking actual pipe dimensions. That shortcut deserves more doubt.
Tips: Check the pipe’s material, diameter, wall thickness, and approved fusion procedure before welding. Keep the heater plate clean and inspect its coating. Record ambient temperature, heating time, joining pressure, and cooling time. Never move the joint during cooling. A neat bead helps, but it is not the only proof of quality. Calibration records and visual inspection should support the final decision.
Top Fusion Welding Machine Manufacturers How to Choose? - What Is a Fusion Welding Machine and How Does It Work?
A fusion welding machine joins compatible thermoplastic components by heating their mating surfaces until they soften, applying controlled contact pressure, and allowing the joint to cool under pressure. The table below summarizes the main machine types, operating data, standards, and manufacturer-selection criteria without listing company or brand names.
| Category | Data Dimension | Typical or Standardized Information | Why It Matters When Choosing a Machine or Manufacturer |
|---|---|---|---|
| What a Fusion Welding Machine Is and How It Works | |||
| Operating principle | Joint formation | Two thermoplastic surfaces are aligned, heated to a molten or softened state, pressed together, and held stationary until the joint cools and solidifies. | The machine must control alignment, temperature, pressure, heating time, changeover time, fusion time, and cooling time. |
| Compatible materials | Common thermoplastics | High-density polyethylene (HDPE), medium-density polyethylene (MDPE), polypropylene (PP), and polyvinylidene fluoride (PVDF), subject to compatible procedures. | Material compatibility, melt behavior, pipe classification, and approved joining procedures must be checked before welding. |
| Basic process sequence | Typical steps | Secure components → face or prepare surfaces → align → heat → remove the heater → bring surfaces together → apply fusion pressure → cool while clamped. | Clear process control reduces misalignment, contamination, insufficient fusion, and excessive bead formation. |
| Heat source | Heating plate or fitting element | Butt-fusion machines generally use a temperature-controlled heating plate. Electrofusion systems use electrically heated fittings with embedded resistance wires. | Uniform heat distribution and stable temperature are essential for repeatable joints. |
| Machine Type and Representative Operating Range | |||
| Socket-fusion machine | Typical outside-diameter range | Approximately 16–110 mm for common portable equipment; the actual range depends on the tool set and material. | Suitable for small-diameter pipe, fittings, plumbing, irrigation, and utility installations. |
| Manual or semi-hydraulic butt-fusion machine | Typical outside-diameter range | Approximately 40–160 mm for compact units and up to roughly 315 mm for larger workshop or field units. | Useful where moderate pipe sizes, portability, and lower equipment cost are priorities. |
| Hydraulic butt-fusion machine | Typical outside-diameter range | Common configurations cover approximately 63–630 mm, with larger specialized systems available. | Hydraulic clamping provides more consistent force for large-diameter or thick-wall pipe. |
| Electrofusion control unit | Input and output requirements | Many systems accept single-phase electrical input and provide controlled voltage, current, and fusion time according to fitting requirements; exact values vary by fitting system. | The unit should support the fitting’s barcode, manual input, voltage, current, and cooling requirements where applicable. |
| Electrofusion machine | Typical application range | Commonly used for PE service connections, repairs, confined spaces, tapping saddles, and joints where butt-fusion access is limited. | Compactness and controlled electrical output can be more valuable than high mechanical clamping capacity. |
| Important Technical Data | |||
| Heating temperature | Typical operating range | PE and PP butt-fusion procedures commonly use a heating plate near 200–230°C. PVDF procedures may require a different range, often around 230–260°C. Always follow the applicable procedure. | Temperature must be verified at the plate surface, not only by the controller display. |
| Temperature control | Control accuracy and stability | A practical specification is closed-loop control with a readable digital display and stable temperature regulation; the required tolerance depends on the governing procedure. | Ask for calibration records, sensor type, control tolerance, and temperature-uniformity test results. |
| Clamping system | Mechanical or hydraulic clamping | Manual clamps are common on small machines; hydraulic clamps are preferred for larger diameters and higher fusion forces. | Clamps should hold the pipe securely without damaging the pipe surface or causing excessive ovality. |
| Alignment capability | Pipe-axis alignment | Adjustable upper clamps, side supports, and controlled facing help keep pipe ends concentric and minimize high-low mismatch. | Poor alignment can reduce weld quality even when temperature and pressure are correct. |
| Facing system | End preparation | Powered or manually driven facing tools remove oxidation, contamination, and uneven pipe ends before heating. | The facer should produce parallel, clean, and square ends without excessive material removal. |
| Pressure control | Fusion-force adjustment | Pressure is determined by the pipe material, outside diameter, wall thickness, SDR, ambient conditions, and the approved joining procedure; there is no single universal pressure value. | Choose equipment with a calibrated pressure gauge or sensor and a method for converting required fusion force into machine pressure. |
| Data recording | Traceability features | Advanced machines may record operator ID, pipe data, temperature, pressure, fusion phases, time, alarms, and joint number. | Data logging is valuable for regulated water, gas, industrial, and infrastructure projects. |
| Power requirements | Electrical supply | Small machines may use standard single-phase power. Larger heaters, hydraulic systems, and electrofusion units may require higher current capacity or a generator. | Confirm voltage, frequency, maximum current, generator sizing, cable length, and site power availability before purchase. |
| Environmental capability | Field operating conditions | Outdoor work may involve wind, rain, dust, low temperature, high temperature, and unstable electrical supply. | Look for protective transport cases, suitable ingress protection, wind shields, low-temperature procedures, and reliable generator compatibility. |
| Standards, Quality, and Manufacturer Evaluation | |||
| Butt-fusion standard | Applicable reference | ASTM F2620 provides guidance for heat-fusion joining of polyethylene pipe and fittings. ISO 21307 defines butt-fusion procedures for polyethylene piping systems. | The machine supplier should explain which procedures and pipe systems the equipment supports. |
| Equipment standard | Fusion-equipment reference | ISO 12176-1 covers equipment for the butt fusion of polyethylene systems. ISO 12176-2 covers electrofusion equipment for polyethylene systems. | Documented conformity and test evidence provide stronger assurance than marketing claims alone. |
| European procedure reference | Industry guidance | DVS 2207 and related DVS guidance are widely referenced for thermoplastic welding procedures, subject to project and regional requirements. | Verify that operating instructions match the standards accepted by the project owner or local authority. |
| Calibration | Measurement traceability | Temperature sensors, pressure gauges, force sensors, timers, and data-recording systems should be calibrated at defined intervals using traceable equipment. | Calibration certificates help demonstrate that process variables were measured accurately. |
| Quality management | Manufacturing controls | Evaluate documented inspection, component traceability, electrical safety testing, hydraulic leak testing, and final machine verification. | A robust quality system can reduce variation between machines and improve spare-parts availability. |
| Operator training | Training and qualification support | Training should cover material identification, surface preparation, heater handling, fusion parameters, cooling, visual inspection, and defect prevention. | Even a high-quality machine cannot compensate for incorrect procedures or poor operator technique. |
| After-sales service | Support capability | Important services include commissioning, troubleshooting, calibration, spare parts, repair turnaround, software support, and technical documentation. | Service availability is especially important for field projects where downtime can be costly. |
| Documentation | Required technical documents | Look for operating manuals, maintenance schedules, electrical diagrams, hydraulic diagrams, spare-parts lists, calibration instructions, and conformity declarations. | Complete documentation supports safe operation, maintenance, audits, and operator training. |
| Practical Selection Checklist | |||
| Project compatibility | Pipe and fitting requirements | Confirm material type, outside-diameter range, wall thickness, SDR, fitting geometry, joint method, and applicable joining procedure. | Choose the machine from actual project requirements rather than maximum advertised capacity alone. |
| Portability | Transport and setup | Consider machine weight, detachable components, lifting points, transport case, setup time, and access to the work area. | A lighter machine may improve productivity on remote or confined sites, while a heavier frame may improve stability. |
| Safety | Protection features | Useful features include insulated heater handles, emergency stop controls, electrical protection, guarded moving parts, pressure relief, and over-temperature protection. | Safety features reduce the risk of burns, crushing injuries, electrical faults, and equipment damage. |
| Total cost of ownership | Purchase and operating cost | Include the machine, tooling, generator, transport, calibration, maintenance, replacement heaters, facing blades, hydraulic components, training, and downtime. | The lowest purchase price may not provide the lowest long-term operating cost. |
| Supplier comparison | Recommended evaluation method | Compare verified specifications, standards compliance, calibration evidence, sample weld records, service response, warranty terms, spare-parts lead time, and user training. | A documented comparison helps identify reliable equipment without relying solely on brand popularity or sales claims. |
Important: Fusion temperature, pressure, heating time, changeover time, fusion time, and cooling time must be selected from the applicable procedure for the specific material, pipe dimensions, SDR, fitting, and environmental conditions. The ranges shown are representative industry values and are not a substitute for the approved joining procedure.