-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose the Right Cordierite Saggar?
Choosing the right Cordierite Saggar is a practical decision, not a simple size comparison. The saggar must suit your kiln, firing schedule, product shape, and loading method. A small mismatch can create cracked corners, warped bases, or uneven heat exposure.
Ceramic kiln-furniture consultant Dr. Michael J. O’Driscoll offers a useful working principle: “The best saggar is the one that survives the full firing cycle without disturbing the product.” This idea keeps attention on real performance. Cordierite is valued for its low thermal expansion and resistance to thermal shock. However, no material is invincible. Repeated heating, cooling, chemical vapors, and rough handling gradually weaken it.
Look closely at the details. Measure the internal length, width, and height, not only the outside dimensions. Leave enough clearance for airflow and product movement. Check the saggar’s wall thickness against its weight and expected service temperature. A thin wall may reduce mass, but it can suffer faster from mechanical damage. A heavy saggar may last longer, yet consume more kiln space and energy.
Surface condition matters, too. Hairline cracks can open during firing. Glaze deposits may build around the rim. Slight distortion can prevent stable stacking. These problems are easy to overlook.
A perfect choice rarely exists. The better approach is to compare actual firing records, supplier data, and maintenance costs. Ask how the Cordierite Saggar performs after repeated cycles, not only when it is new. Careful selection begins with honest observation.
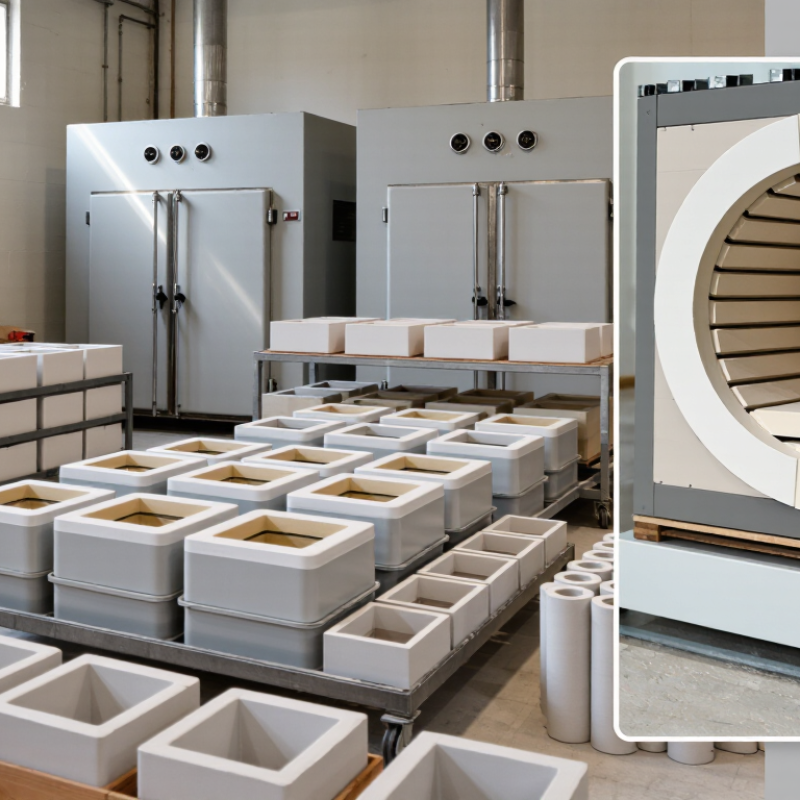
Table of Contents [Hide]
Define the Material and Firing Requirements
How to Choose the Right Cordierite Saggar?
Define the Material and Firing Requirements
When choosing a cordierite saggar, define the firing job before comparing dimensions or price. Cordierite is valued for low thermal expansion and strong thermal-shock resistance. However, formulations vary. Ask for the cordierite content, apparent porosity, bulk density, and maximum recommended temperature. A dense saggar may resist abrasion better. A more porous body may respond differently to thermal changes. That trade-off deserves attention.
Record the kiln’s peak temperature, heating rate, cooling rate, and atmosphere. Include the number of cycles expected each week. A saggar used near 1,200°C faces different demands from one used near 1,400°C. Do not rely on peak temperature alone. Uneven loading, tight stacking, and direct flame exposure can create local stress. Leave clearance between saggars and kiln walls. Small gaps matter. Also define the payload: powder, pellets, glazed parts, or technical ceramics. Reactive materials may affect the selection.
Before full production, run a controlled trial with representative loads. Measure warpage, cracks, edge chipping, and contamination after several cycles. Compare the saggar’s weight and dimensions before and after firing. Keep a simple firing log. It can reveal patterns that memory misses. A common mistake is treating one successful firing as proof of reliability. That assumption is incomplete. Longer cycling may expose problems later. Request inspection records and test data, then match them to your actual kiln conditions. The right saggar fits the process, not just the catalogue.
How to Choose the Right Cordierite Saggar? - Define the Material and Firing Requirements
| Selection Dimension | Typical Requirement or Range | Why It Matters | Recommended Saggar Specification |
|---|---|---|---|
| Firing Temperature | Approximately 1,000–1,300 °C for many ceramic and powder-processing applications | The saggar must retain its shape and strength throughout repeated heating cycles. | Select a cordierite grade with a published continuous-use temperature at or above the actual kiln temperature, including operating margin. |
| Thermal Expansion | Typically about 1.5–3.0 × 10⁻⁶/K from room temperature to approximately 1,000 °C, depending on composition and processing | Low expansion helps reduce cracking caused by rapid temperature changes. | Use low-expansion cordierite when the kiln cycle includes fast heating, fast cooling, or frequent loading and unloading. |
| Thermal-Shock Exposure | High exposure: rapid heating or cooling, short cycle times, or direct transfer between hot and cooler zones | Thermal gradients can create tensile stress, especially at corners, edges, and uneven wall sections. | Choose uniform wall thickness, rounded internal corners, smooth edges, and a verified low-expansion cordierite formulation. |
| Firing Atmosphere | Air, oxidizing, neutral, or reducing atmosphere according to the product process | Atmosphere can affect the load, surface deposits, saggar durability, and cleaning frequency. | Confirm chemical compatibility with the process atmosphere, fuel products, vapors, and any protective powders used inside the saggar. |
| Chemical Compatibility | Exposure may include alkaline, acidic, metallic, glassy, or volatile process materials | Chemical attack can cause surface erosion, sticking, contamination, or premature failure. | Request compatibility data for the specific load chemistry; use a compatible setter powder, wash, or liner when required. |
| Saggar Wall Thickness | Common light- to medium-duty ceramic saggars: approximately 8–20 mm; larger or heavily loaded designs may require more | Thicker walls improve rigidity but increase thermal mass, heating time, and thermal gradients. | Select the thinnest wall that safely supports the load and survives handling, stacking, and the planned firing cycle. |
| Size and Load Distribution | Load should be distributed evenly without concentrated weight or unsupported spans | Uneven loading can cause warping, cracking, and contact between the product and saggar walls. | Allow clearance around the load, avoid overfilling, and use a reinforced base or ribs for large footprints when appropriate. |
| Stacking and Kiln Fit | Stacking height and spacing must match kiln clearance and saggar load capacity | Poor stacking can obstruct airflow, create uneven heating, or overload lower saggars. | Verify external dimensions, flatness, corner clearance, support-point alignment, and the maximum safe stacked load. |
| Flatness and Dimensional Stability | Important for long, wide, thin, or repeatedly stacked saggars | Warping may reduce usable volume, destabilize stacks, and cause product damage. | Specify allowable flatness, squareness, and dimensional tolerances based on the product and kiln layout. |
| Surface Finish and Release | Smooth, cleanable surfaces are preferred for loads that may adhere during firing | A suitable surface reduces sticking, contamination, chipping, and product removal damage. | Choose a suitable finish or compatible kiln wash; inspect and renew the release layer according to actual wear. |
| Expected Service Life | Depends on temperature, cycle rate, loading, atmosphere, chemical exposure, and handling | A lower purchase cost may be offset by frequent replacement and process interruptions. | Track cracks, warping, erosion, and contamination; remove saggars before defects can affect product quality or kiln safety. |
Note: The values shown are typical engineering guidance for cordierite ceramic saggars. Actual limits vary with formulation, density, geometry, manufacturing method, kiln atmosphere, and firing cycle; always verify the technical data for the selected saggar design.