-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top 10 Idler Arm Manufacturers How to Choose?
Choosing among China’s top 10 Idler Arm manufacturers requires more than comparing prices. This steering component supports linkage movement and helps maintain accurate wheel control. A poorly matched part may create looseness, uneven tire wear, or unstable handling. For that reason, buyers should examine design capability, material quality, machining accuracy, and inspection procedures together.
A reliable manufacturer should explain its production process clearly. Look for forged or cast material specifications, heat-treatment records, dimensional reports, and load-testing methods. Ask whether the Idler Arm matches the vehicle’s original geometry, mounting points, and bushing requirements. Factory experience also matters. A supplier serving commercial trucks may not understand the needs of passenger vehicles or specialty platforms. Small details matter here, including grease fitting placement, thread protection, and corrosion-resistant finishing.
The phrase “top 10” should not be treated as a permanent ranking. Manufacturing capacity, certifications, export performance, and customer service can change. Buyers should verify company information through factory audits, sample testing, and recent customer references. One sample is not enough. Request several units and compare hardness, joint movement, surface finish, and installation fit. It is also wise to review warranty terms, packaging strength, lead times, and technical support before signing a contract.
No supplier is perfect. Even an experienced factory can show inconsistent batches or unclear documentation. Careful questioning exposes those weaknesses early. This guide compares ten Chinese Idler Arm manufacturers through practical criteria, helping importers balance quality, cost, reliability, and long-term support. The best choice is not always the cheapest. It is the supplier that can repeatedly deliver safe, traceable, and correctly engineered components.
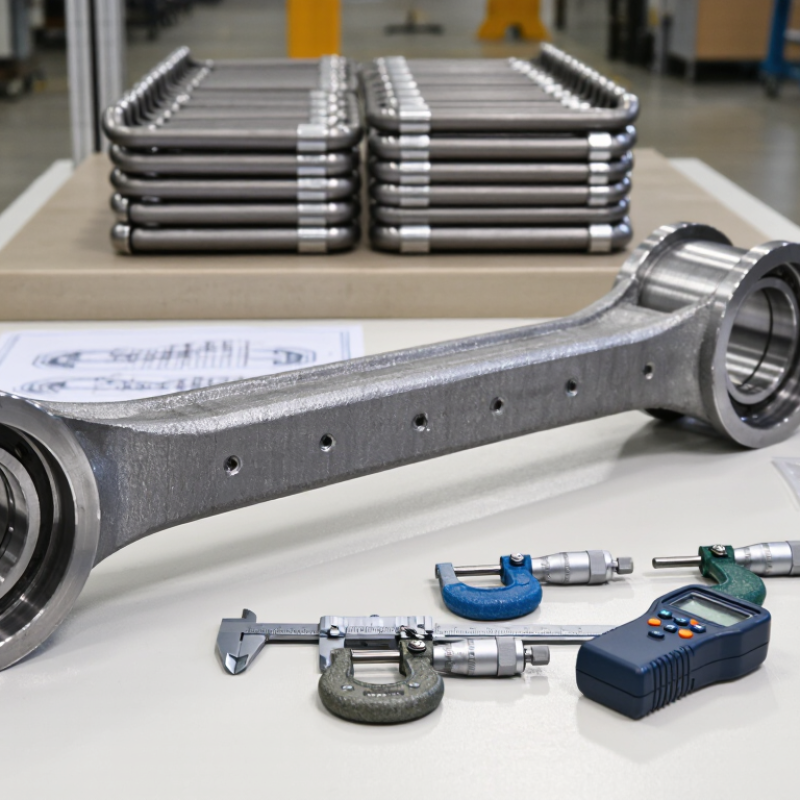
Table of Contents [Hide]
What Is an Idler Arm and Why Does It Matter?
An idler arm is a steering-linkage component used in many rear-wheel-drive vehicles. It supports the center link opposite the pitman arm. Together, these parts guide the front wheels as the driver turns the steering wheel. The idler arm does not create steering movement. It keeps the linkage aligned and helps control its vertical motion. That quiet support role is easy to overlook.
During workshop inspections, technicians often check for excessive play, damaged bushings, loose mounting points, and uneven movement. A worn idler arm may cause vague steering, wandering, clunking sounds, or irregular tire wear. However, one symptom does not prove failure. A quiet test drive can still hide serious looseness. A proper inspection should combine hands-on checks, linkage measurement, and a review of tire patterns.
Choosing an idler arm manufacturer requires more than comparing prices. Look for accurate original-equipment dimensions, forged or suitably strengthened materials, protected joints, and bushings that resist road moisture. Clear load testing, corrosion testing, batch traceability, and practical warranty terms show stronger quality control. Greaseable joints can support longer service in harsh conditions, but they still need maintenance. Some product descriptions sound impressive. The details matter more. Confirm vehicle fitment, steering geometry, and installation torque before purchase. A reputable supplier should provide technical data rather than vague durability claims.