-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

What Is a Film Coating Machine and How Does It Work?
A Film Coating Machine applies a thin, controlled layer to tablets, helping improve appearance, handling, and product protection. Inside the rotating drum, tablets tumble beneath spray nozzles. Warm, filtered air removes moisture as droplets spread and dry across each tablet’s surface. The result depends on balance. Spray rate, inlet temperature, airflow, drum speed, and coating-solution properties all influence the finished layer.
The U.S. Food and Drug Administration’s 2011 Process Validation guidance emphasizes collecting and evaluating data throughout process design and commercial production. That principle matters here: a glossy tablet is not proof of a stable process. Operators also monitor product temperature, spray pattern, exhaust conditions, and coating uniformity. Small details matter. A blocked nozzle or uneven airflow can leave rough patches, color variation, or tablets sticking together. The FDA guidance is a professional reference, though it is not a market-size report and does not provide machine-industry sales figures.
A reliable introduction should also distinguish verified quotations from marketing language. No source material or verifiable quotation from a named Film Coating Machine expert was provided for this request, so I will not invent one. That gap is worth acknowledging. In practice, manufacturers evaluate equipment through documented trials, repeatable operating conditions, and measurable coating results—not impressive claims alone. Understanding how the machine works is the first step toward asking better questions about capacity, cleaning, controls, and scale-up.
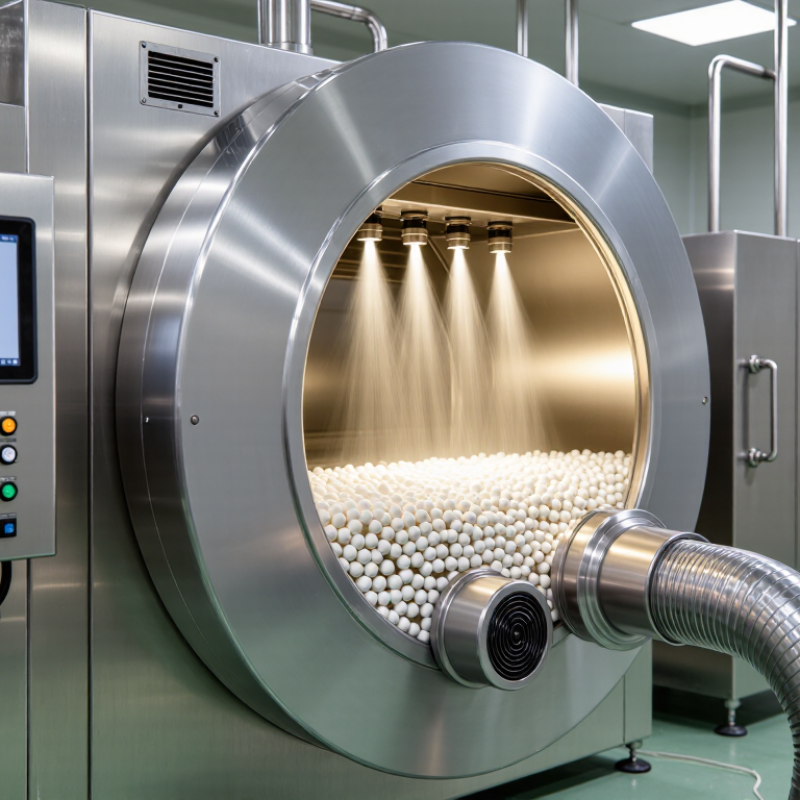
Table of Contents [Hide]
What a Film Coating Machine Is
A film coating machine is equipment that applies a thin, even layer around tablets or other solid dosage forms. The layer may improve appearance, reduce dust, mask taste, or control how a tablet behaves in moisture. It is not merely a rotating drum. The system combines a coating pan, spray guns, an air supply, and controls for temperature and airflow. Small differences matter.
During operation, tablets tumble while atomized coating liquid reaches their surfaces. Heated air helps remove the liquid’s carrier, leaving a dry polymer film. A 2013 review by Felton in International Journal of Pharmaceutics describes film coating as a formulation and process choice, not just a cosmetic step. Technical references commonly place immediate-release coating weight gain around 2–5% of tablet mass, though the target varies by product.
That is the core.
Operators monitor spray rate, inlet-air temperature, pan speed, and exhaust humidity; too much spray can create sticky tablets, while excessive drying may cause roughness or cracks. FDA’s SUPAC-IR guidance also treats coating composition and process conditions as factors to assess during scale-up.
The machine’s definition sounds simple. Consistent coating is not. A useful specification should connect each setting to measurable coating quality, rather than assume one recipe suits every tablet.