-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose Welded Stainless Steel Pipe?
A Welded Stainless Steel Pipe may look like a simple metal cylinder, but choosing one involves more than comparing price and diameter. The International Stainless Steel Forum’s Stainless Steel in Figures 2024 reports global stainless steel production of 58.4 million tonnes in 2023. That scale reflects broad industrial use, not a guarantee that every pipe suits every job. A line carrying clean water has different demands from one exposed to chlorides, heat, or frequent pressure changes.
Start with the service conditions. Record the fluid, operating temperature, pressure, and exposure to chemicals. Then check the grade, outside diameter, wall thickness, weld quality, and required finish. ASTM A312/A312M covers welded and seamless austenitic stainless steel pipe for high-temperature and general corrosive service. ASTM A778 covers certain welded, unannealed austenitic tubular products. The exact specification matters; “stainless” alone is not a sufficient purchasing description.
Ask suppliers for material test reports, traceability, and inspection details. Match these records to the ordered grade and dimensions. Look closely at the weld seam and cut ends, especially when the pipe will be installed in a wet or corrosive area. A polished surface can be reassuring. It cannot prove suitability. That is easy to overlook. Even experienced buyers can focus too much on alloy names and miss fabrication details. Use the project specification and qualified technical advice to resolve uncertainties before ordering. A careful choice begins with the actual service, not a catalog photograph.
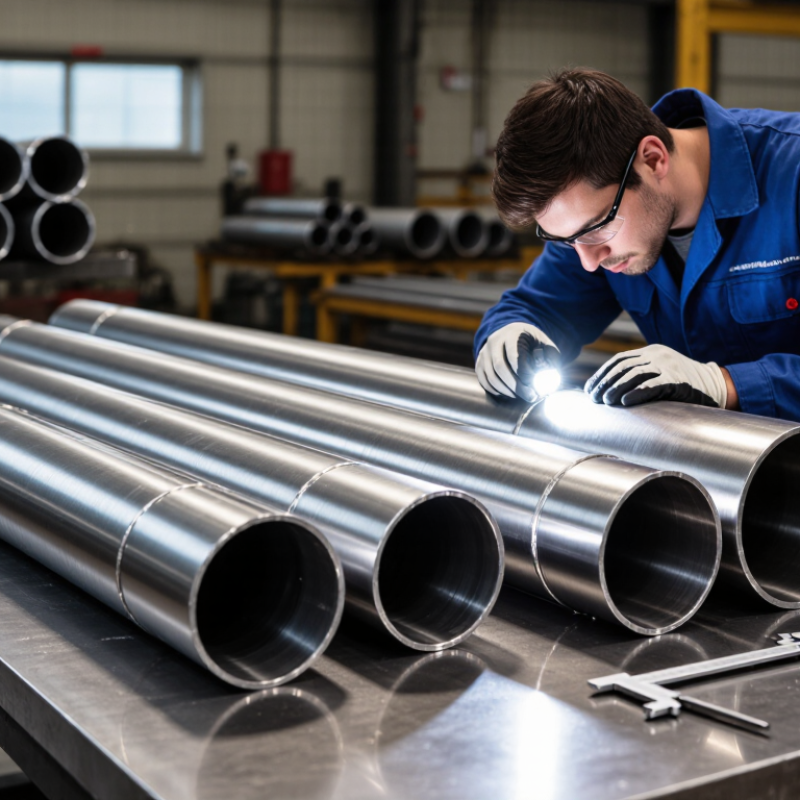
Table of Contents [Hide]
Define the Pipe’s Application and Operating Conditions
Choosing welded stainless steel pipe starts with service definition, not diameter. Record fluid, concentration, temperature, pressure, flow, and cleaning chemicals. Note whether the line carries drinking water, steam, chemicals, or abrasive slurry. ASME B31.3 links pipe design to pressure, temperature, materials, fabrication, and testing. A pipe suited to 20°C water may fail in hot chloride service. Small details matter. Include startup shocks and vacuum conditions.
The corrosion environment deserves measurable attention. Chlorides, low pH, stagnant pockets, and wet-dry cycling can attack weld areas. NACE’s IMPACT study estimated global corrosion costs at about US$2.5 trillion annually, equal to 3.4% of global GDP. That figure supports disciplined selection, not automatic use of a higher alloy. Ask for chloride limits, oxygen exposure, and expected service life. For a 90°C process line at 16 bar, specify the actual fluid chemistry, not merely “industrial water.” A site survey should inspect dead legs, supports, drain points, and heat-affected zones.
Match the specification to fabrication reality. ASTM A312 covers seamless and welded austenitic stainless pipe. Project requirements should define grade, wall thickness, weld procedure, inspection, and pressure testing. Experienced engineers also check thermal expansion and repeated cycling. Field reviews often reveal tidy drawings hiding uncertain cleaning practices. That weakness matters. If operators may use strong cleaners, record concentration and contact time. Outdoor lines need evaluation for rainwater, insulation traps, and coastal salt. Reconsider the choice when operating data is missing; confident assumptions are still assumptions.
How to Choose Welded Stainless Steel Pipe? — Define the Pipe’s Application and Operating Conditions
Use this table as a preliminary selection guide. Final pipe grade, dimensions, wall thickness, welding requirements, pressure rating, and inspection level must be verified against the applicable design code, process conditions, and governing product standard.
| Application | Typical Service Medium | Operating Temperature Considerations | Corrosion Environment | Common Stainless Steel Options | Recommended Product Standard | Weld and Surface Requirements | Key Selection Checks |
|---|---|---|---|---|---|---|---|
| General water, air, and low-corrosive utility piping | Potable water, treated water, compressed air, inert gas | Normally ambient to moderately elevated temperatures; confirm thermal expansion where temperature changes are frequent. | Low chloride exposure and limited chemical contamination | 304L for general corrosion resistance; 316L where chlorides or mild chemical exposure are present | ASTM A312 or EN 10217-7, depending on project requirements | Continuous longitudinal weld; pickled and passivated surfaces are commonly specified after fabrication. | Check water chemistry, chloride content, sanitary requirements, nominal diameter, wall thickness, and joining method. |
| Food, beverage, and hygienic process lines | Water, milk-based liquids, oils, syrups, cleaned-in-place solutions | Ambient service with repeated hot-water, steam, or cleaning cycles | Organic acids, cleaning chemicals, moisture, and frequent wet-dry cycles | 304L for less aggressive service; 316L for higher chloride or chemical exposure | ASTM A270 for sanitary tubing applications; ASTM A312 or EN 10217-7 for process piping where applicable | Internal weld bead control, low-roughness finish, full drainage, orbital or high-quality TIG welding, and passivation are commonly required. | Specify internal surface roughness, hygienic fittings, dead-leg prevention, cleanability, drainability, and weld inspection. |
| Seawater and coastal cooling systems | Seawater, brackish water, seawater cooling water | Temperature, flow velocity, oxygen content, and stagnant zones strongly affect service life. | High chlorides, deposits, crevices, and possible pitting or crevice corrosion | 316L may be suitable for limited conditions; higher-alloy stainless steels or non-stainless alloys may be required for severe seawater exposure. | Project-specific piping specification; ASTM A312 or ASTM A358 may be considered where applicable | Use high-quality welds with careful heat control; remove heat tint and passivate surfaces after welding. | Evaluate chloride concentration, velocity, oxygenation, biofouling, crevice design, galvanic coupling, and corrosion allowance. |
| Moderate-temperature chemical processing | Dilute acids, alkaline solutions, solvents, and process chemicals | Temperature increases can significantly accelerate corrosion; consider start-up, shutdown, and cleaning conditions. | Chemical concentration, pH, chlorides, oxidizing agents, and contaminants determine suitability. | 316L is often considered for improved molybdenum-enhanced pitting resistance; the exact chemical compatibility must be confirmed. | ASTM A312, ASTM A358, or EN 10217-7 according to pressure, diameter, and project specification | Control weld heat input, minimize sensitization risk, remove weld discoloration, and specify suitable non-destructive examination. | Obtain corrosion data for the exact chemical, concentration, temperature, flow condition, and exposure time before approval. |
| High-temperature process and exhaust service | Hot air, combustion products, process gases, and heated fluids | Continuous and cyclic high-temperature exposure; thermal fatigue and oxidation must be considered. | Oxidizing gases, carburizing conditions, sulfur compounds, or condensates may affect alloy selection. | 321 or 347 may be selected for improved resistance to intergranular corrosion after exposure to elevated temperatures; service-specific verification is required. | ASTM A312 or ASTM A358, subject to design code and fabrication requirements | Use qualified welding procedures, control distortion, and consider post-weld cleaning and heat-treatment requirements. | Check design temperature, thermal cycling, oxidation, creep considerations, expansion loads, insulation, and support spacing. |
| Steam and pressurized hot-water systems | Steam, condensate, boiler feedwater, hot process water | Temperature and pressure may vary significantly during start-up and shutdown. | Dissolved oxygen, chlorides, scaling, erosion, and condensate chemistry | 304L or 316L may be considered depending on water chemistry and design temperature. | ASTM A312 or another pressure-piping standard required by the applicable code | Weld quality, dimensional control, radiographic or ultrasonic examination, and hydrostatic or alternative pressure testing may be specified. | Calculate wall thickness using the governing code; verify allowable stress, pressure-temperature rating, supports, and thermal expansion. |
| Architectural, structural, and exposed outdoor service | Rainwater, humid air, atmospheric exposure, decorative or structural applications | Ambient temperature with possible solar heating and freeze-thaw cycles | Urban pollutants, coastal salt spray, moisture retention, and crevice contamination | 304 for many inland environments; 316 is commonly considered for coastal or chloride-containing atmospheres. | ASTM A554 for ornamental or mechanical tubing; ASTM A312 where pressure service applies | Specify visible weld appearance, grinding or polishing level, pickling, passivation, and protection against embedded iron contamination. | Assess atmospheric severity, drainage, crevices, finish, cleaning frequency, dimensional tolerance, and load requirements. |
| Underground or buried process piping | Water, wastewater, chemicals, and industrial process fluids | Soil temperature, seasonal variation, and freeze protection may be relevant. | Soil chlorides, sulfates, moisture, stray currents, and external corrosion | 304L or 316L may be considered only after soil and fluid conditions are evaluated. | ASTM A312, ASTM A358, or the applicable regional pressure-piping standard | Use qualified field welding procedures, external protection where required, and inspection of coating or wrapping systems. | Evaluate soil resistivity, drainage, cathodic protection, external coating, accessibility, settlement, and leak detection. |