-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose the Right U Panel Machine?
Choosing the right U Panel Machine is a production decision, not merely a purchase. It affects panel strength, line speed, material waste, and daily operating costs. In my experience, buyers often focus on the quoted price and overlook tooling accuracy, roll-forming stability, and service response. That mistake can become visible in every uneven seam.
A dependable evaluation begins with the intended panel specification. Confirm the panel width, rib profile, steel thickness, coating type, and required output. Then examine the machine’s forming stations, drive system, cutting method, and control interface. Ask for sample panels made from comparable material. Inspect their edges, dimensions, surface marks, and joint fit. Small defects matter. A panel that looks acceptable at low speed may fail during continuous production.
Manufacturers should provide measurable data, maintenance guidance, electrical documentation, and realistic capacity figures. Independent references can reveal more than polished brochures. Speak with operators who have used similar equipment for several seasons. They can explain setup time, spare-part availability, and common service delays. Still, no machine is perfect. A highly automated line may improve consistency but require stronger technical support. A lower-cost model may suit modest production, yet limit future expansion. This guide examines those trade-offs carefully, helping you compare performance, reliability, safety features, and long-term value before choosing a U Panel Machine.
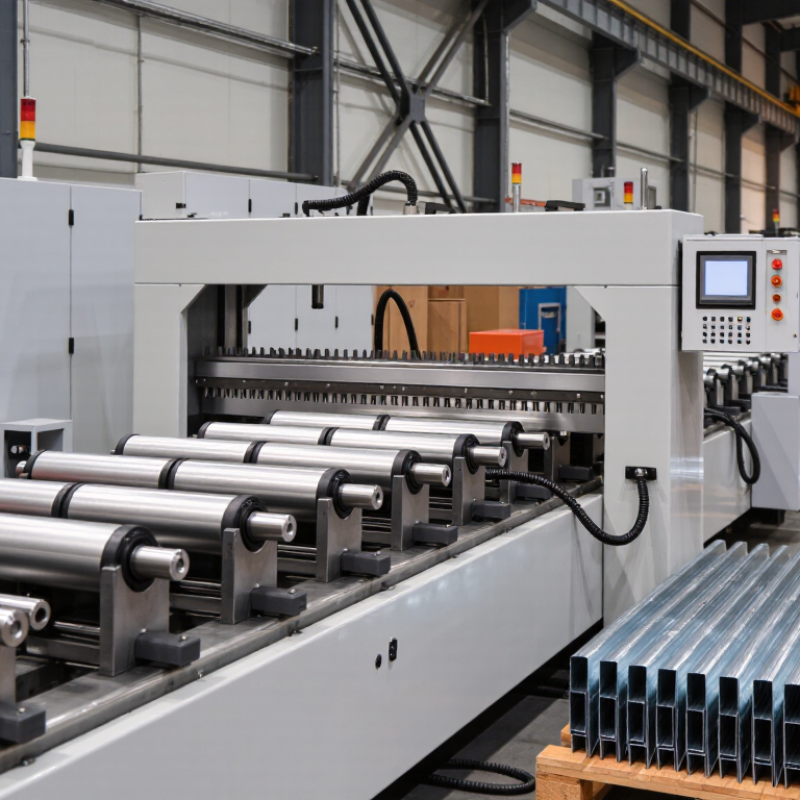
Table of Contents [Hide]
Define U-Panel Profiles: Width, Depth, Gauge, and ASTM A653 Steel Grade
How to Choose the Right U Panel Machine?
Before selecting a U panel machine, define the profile precisely. Record the panel width, sidewall depth, return-lip size, and overall height. These measurements control roll tooling, machine clearance, and forming stability. Do not rely on a sketch alone. A small dimensional error can produce poor joints or uneven panel edges.
Gauge needs equal attention. In many markets, gauge refers to thickness, but its meaning can vary. Confirm the actual millimeter thickness with the supplier and check the permitted tolerance. Thicker steel usually demands stronger forming stands and greater drive capacity.
However, thicker is not always better. It can increase cost, springback, and adjustment time.
ASTM A653/A653M identifies hot-dip zinc-coated steel sheet and related requirements. Specify the steel grade, coating designation, yield strength, and finish before discussing machine speed. Commercial steel forms differently from structural grades. Coating weight also affects surface protection and roll contact.
Ask for material certificates and test samples. Real production trials matter.
I have seen attractive specifications fail when the coil hardness differed from the sample. The mistake was not dramatic, but it was expensive. Leave room for setup corrections, because real coils rarely behave perfectly.