-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

7 Tips for Choosing the Best MCB Riveting Machine
Selecting the right Mcb Riveting Machine affects terminal strength, cycle time, safety, and long-term maintenance costs. A small riveting error can loosen an electrical connection inside an MCB. The result may be difficult to detect during final inspection.
Industry data supports careful evaluation. Grand View Research’s 2024 circuit breaker market analysis identifies automation, reliability, and electrical safety as major development priorities. MarketsandMarkets also reports continuing investment in circuit protection manufacturing through smart factories and higher production efficiency. These trends make machine selection more than a price comparison. It becomes a quality decision.
This guide presents seven practical tips for choosing the best Mcb Riveting Machine. The recommendations focus on rivet consistency, tooling accuracy, feeding stability, production speed, and operator protection. They also consider changeover time and after-sales support. Important details include spindle alignment, adjustable riveting pressure, sensor response, and rejected-part control. Ask for sample testing. Numbers matter.
A supplier should provide measurable results, not only attractive photographs. Request cycle-time records, repeatability data, maintenance instructions, and references from comparable production lines. ISO 9001-based quality processes can strengthen supplier credibility, while IEC 60898-1 remains a useful reference for low-voltage circuit-breaker requirements. However, compliance alone does not guarantee a suitable machine. That assumption is risky.
No machine is perfect. Real factories contain dust, operator variation, worn tooling, and unexpected material changes. A thoughtful buyer tests these conditions before signing. The best decision balances technical performance, documented experience, total ownership cost, and dependable service. A cheaper machine may become expensive when every adjustment stops production.
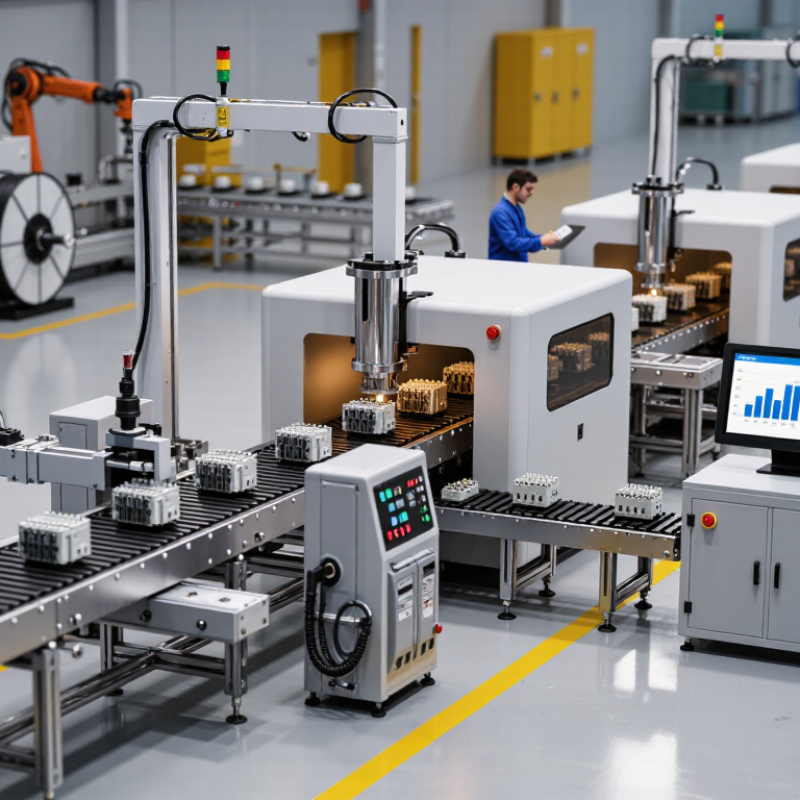
Table of Contents [Hide]
Define MCB Riveting Requirements and Production Goals
Before comparing an MCB riveting machine, define the exact job it must perform. Record breaker dimensions, rivet diameter, material, head shape, and acceptable joint height. Measure the required force with trial assemblies, not estimates from a catalog. Small errors can loosen a terminal or damage the housing. Keep samples nearby.
Production goals should include hourly output, shift length, changeover time, and rejection limits. Specify whether operators load parts manually or use automatic feeding. Ask for controlled stroke depth, adjustable pressure, and repeatable positioning. For quality assurance, require process records, sample checks, and accessible maintenance points. Cycle time matters. Yet speed alone misleads.
In practice, test the machine with your actual MCB components and rivets. Check noise, vibration, alignment, and jam recovery during a full production simulation. A machine may meet its advertised output but fail during frequent size changes. I have seen teams overvalue peak speed and overlook feeding interruptions. That assumption deserves questioning. Let operators review loading height, controls, guarding, and cleaning access. Document every result before selecting equipment.