-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose Borosilicate Glass Sheet in 2026?
Choosing a Borosilicate Glass Sheet in 2026 requires more than comparing thickness and price. The right sheet must match heat, light, chemical exposure, and mechanical demands. A laboratory enclosure, oven window, solar component, and architectural panel may all need different glass grades.
Dr. James E. Shelby, a recognized glass science researcher, offers a useful principle: “Glass performance begins with composition, not appearance.” That statement deserves attention. A perfectly clear sheet can still fail after repeated thermal cycling. Small bubbles, edge chips, uneven thickness, or poor surface finishing can become serious weaknesses. Look closely.
Begin with the thermal expansion coefficient. Low expansion reduces cracking when temperatures change rapidly. Confirm the maximum continuous temperature, short-term temperature resistance, and thermal-shock performance. These figures should come from technical data, not sales language alone. Check them carefully.
Chemical durability also matters. Borosilicate Glass Sheet may resist water, acids, and laboratory chemicals, but resistance varies with formulation and exposure time. Ask for test methods, tolerances, and traceable batch information. Vague certificates are not enough.
Thickness selection needs practical judgment. Thicker glass improves stiffness, yet it adds weight and may complicate cutting or mounting. Larger panels need stronger support and better edge protection. This is often underestimated.
Optical quality can be decisive. Inspect haze, transmission, scratches, waviness, and coating compatibility under real lighting. Some projects overvalue perfect clarity while ignoring installation stress. That can be an expensive mistake.
A reliable supplier should provide samples, inspection records, packaging details, and responsive technical support. Compare the sheet after processing, not only before delivery. Specifications help, but field conditions can expose assumptions that looked reasonable on paper.
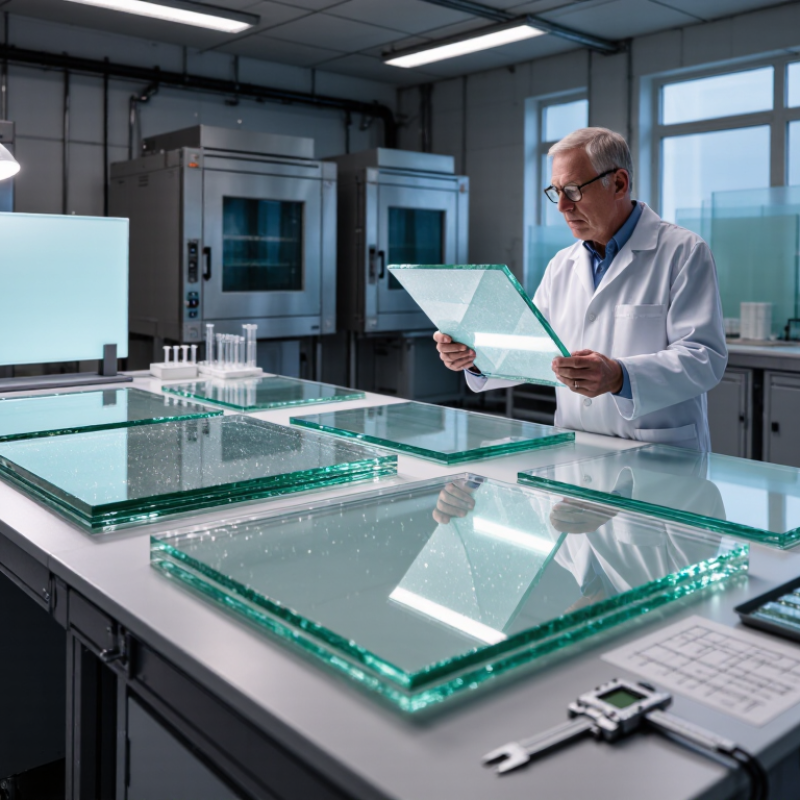
Table of Contents [Hide]
What Is Borosilicate Glass and Why Choose It in 2026?
How to Choose Borosilicate Glass Sheet in 2026?
Borosilicate glass contains boron oxide, which lowers thermal expansion compared with ordinary soda-lime glass. It handles sudden temperature changes more reliably. A hot laboratory tray can meet a cool metal bench with less stress. It also resists many chemicals, making it useful for laboratory equipment, viewing windows, lighting covers, and precision instruments. It is not magic. Excessive impact can still cause failure.
In 2026, choose the sheet according to its real working conditions. Check operating temperature, temperature cycling, chemical contact, thickness, dimensions, and edge treatment. A thin sheet may improve light transmission, but a thicker sheet can provide better rigidity. Ask for thermal expansion data, optical specifications, flatness tolerances, and inspection records. Reliable suppliers should explain testing methods, not only provide attractive product photos. I have found that unclear edge quality often creates problems during cutting and installation.
Consider the complete design, not only the glass itself. Sharp corners, uneven frames, and concentrated fastening pressure may produce stress points. Rounded edges and flexible gaskets usually reduce local damage. If the sheet will face repeated heating, request thermal-shock testing under conditions close to actual use. A specification that looks excellent on paper may still be unsuitable in practice. Recheck the decision after a small prototype, because real assembly pressure can reveal weaknesses early.