-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose a High Speed Diaper Packing Machine?
Choosing the right High-speed diaper packing machine is not simply a speed comparison. It is a production decision involving hygiene, accuracy, labor, materials, and long-term reliability. A machine may advertise 600 packs per minute, yet real output can fall when diaper sizes change or film tension varies. Numbers need context.
In practical factory evaluations, I would inspect the complete packaging process, not only the main frame. Watch how products enter the feeding system. Check whether packs remain aligned during compression. Examine sealing edges, date coding, film tracking, and finished-pack handling. Small defects become expensive when repeated across thousands of packs. The machine should also support stable operation, quick size adjustment, and accessible maintenance points. Operators should understand these functions without relying on guesswork.
Safety and compliance deserve equal attention. Confirm electrical standards, guarding, emergency stops, documentation, and sanitation requirements for the intended market. Ask for recorded test results, sample packs, spare-parts information, and references from comparable facilities. A supplier’s response to difficult questions often reveals more than its brochure. Do not trust speed alone. It can be misleading.
There is no perfect machine. A faster model may require more skilled maintenance or higher film quality. A lower-cost option may create hidden downtime. Buyers should compare total ownership costs, including energy, training, waste, service, and future expansion. I may overlook a detail without a site visit, so every recommendation should remain open to verification. The best choice balances proven performance, product protection, operator safety, and realistic factory needs.
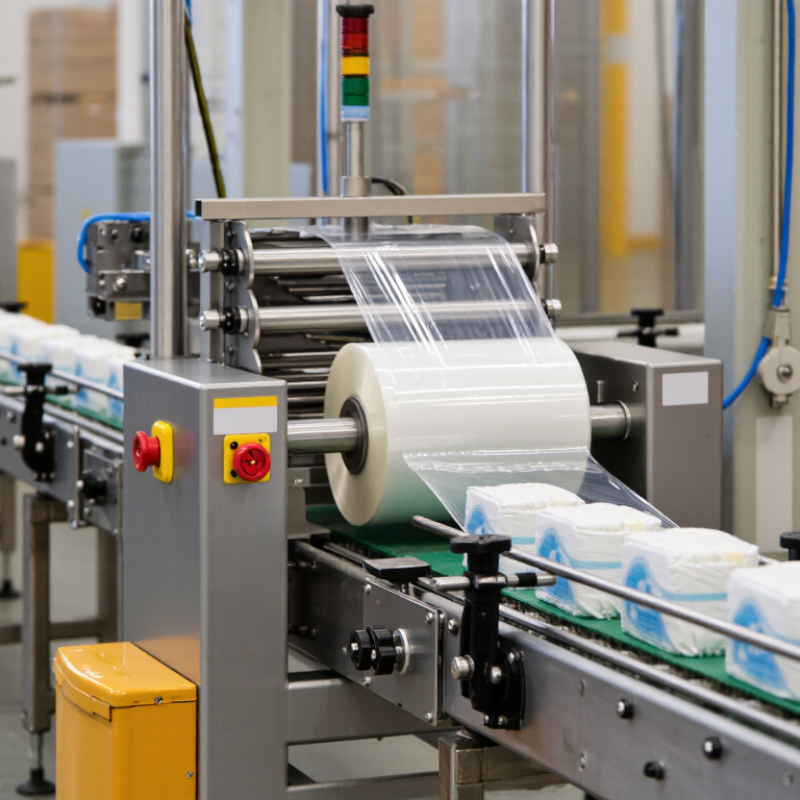
Table of Contents [Hide]
Define High-Speed Performance: 60–120 Diaper Packs per Minute
How to Choose a High Speed Diaper Packing Machine?
Define High-Speed Performance: 60–120 Diaper Packs per Minute
A high-speed diaper packing machine typically handles 60–120 packs per minute. However, this figure is rarely constant in daily production. Actual speed depends on diaper size, pack count, film thickness, and folding accuracy. A machine running at 120 packs per minute may slow to 80 when producing larger bundles. Speed is conditional.
In factory trials, measure sustained output rather than the highest screen value. Watch the infeed conveyor, stacking unit, sealing jaws, and discharge section for at least one hour. Record stoppages, rejected packs, film breaks, and operator adjustments. Measure it live. A reliable machine should maintain stable seals and neat edges at the selected speed. Loose wrapping can damage transport efficiency and customer confidence.
A practical evaluation also includes changeover time. Switching from a small newborn pack to a larger economy pack should not require excessive manual alignment. Ask for test data using your own diaper dimensions and packaging materials. Check whether the quoted 60–120 packs per minute includes rejected products or only accepted packs. That detail matters. Some specifications look impressive but hide frequent micro-stops. I have seen fast equipment lose production through small sensor delays and awkward cleaning access. This is easy to overlook. Choose performance that workers can repeat safely, not merely a peak number recorded during a short demonstration.