-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top Custom Zinc Alloy Die Casting Manufacturer
China’s manufacturing strength is changing how global buyers evaluate Custom Zinc Alloy Die Casting. Price still matters, but it no longer tells the whole story. Consistent dimensions, clean surfaces, and dependable delivery matter more.
Dr. Frank C. Goodwin, a recognized zinc-industry specialist, has stated, “Zinc combines precision, productivity, and recyclability when its process is controlled.” That principle reflects real production conditions. A skilled manufacturer checks alloy composition, mold temperature, injection speed, and filling pressure. Small changes can affect porosity, flash, and surface texture. A thin phone bracket may require different controls than a heavy automotive housing. Details decide performance.
The best Chinese suppliers connect engineering support with disciplined factory work. They review 3D drawings, identify difficult corners, and recommend practical wall thicknesses. They also inspect first articles before full production. This reduces expensive surprises. Traceable material records and dimensional reports add confidence for international customers. The process should include pressure testing, visual checks, and sampling plans when the component requires them.
No factory gets every shot perfect. That is the uncomfortable truth. Even experienced teams can miss a minor burr or underestimate a coating issue. Reliable manufacturers respond with corrective action, not vague promises. Buyers should ask about tooling life, zinc alloy grades, quality certificates, packaging methods, and after-sales support. Custom Zinc Alloy Die Casting is not merely a casting service. It is a controlled partnership between design, tooling, production, and inspection. When those parts work together, a China-based supplier can deliver precise components with competitive value and repeatable quality.
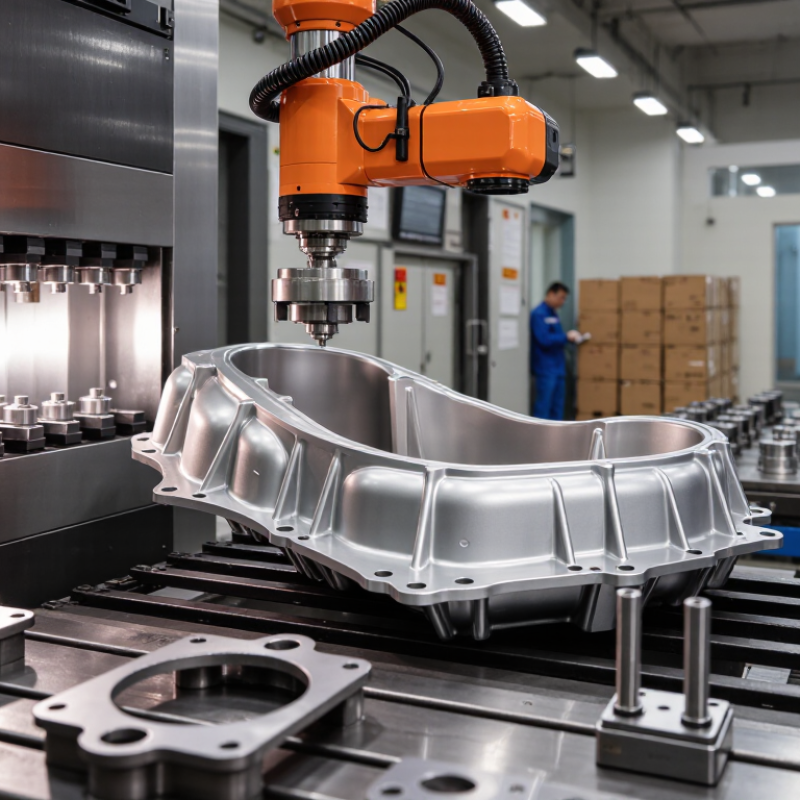
Table of Contents [Hide]
China’s Custom Zinc Alloy Die Casting Manufacturing Overview
China Top Custom Zinc Alloy Die Casting Manufacturer
China’s Custom Zinc Alloy Die Casting Manufacturing Overview
China has a mature zinc alloy die casting supply chain, supported by mold makers, casting plants, and finishing workshops. Custom production usually begins with a 3D design review and flow simulation. Engineers check wall thickness, draft angles, ejector locations, and likely air entrapment before cutting the mold.
Hot-chamber machines are common for zinc alloys because they support fast, repeatable cycles. Zinc flows into detailed cavities and can produce thin walls, textured surfaces, and clean threads. After casting, parts may receive trimming, drilling, polishing, plating, or powder coating. A dependable manufacturer records melt temperature, injection pressure, cycle time, and dimensional results. These records help explain variation instead of hiding it.
Tips: Share the 3D file, material grade, annual quantity, and surface expectations early. Ask for first-article samples and a written inspection plan. Small design changes can reduce flash and extend mold life. Do not judge a supplier by equipment size alone. Communication, traceability, and corrective action matter more than impressive photographs.
Cost remains important, but low tooling prices can create later problems. Poor venting may leave pinholes or weak edges. Uneven cooling can cause distortion. No process is flawless. Experienced teams still review rejected samples, question assumptions, and improve the next production run. For overseas buyers, clear packaging details and pre-shipment inspection also protect consistency during delivery.