-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Which Is China Top Ceramic Irregular Nozzle Manufacturer?
Choosing the right Ceramic Irregular Nozzle Manufacturer requires more than comparing product photos or advertised prices. Irregular nozzles often guide abrasive slurries, molten materials, gases, or highly concentrated fluids. Their uneven channels can create pressure changes, dead zones, and unexpected wear. A reliable supplier must understand those details before recommending a design.
Dr. Elena Morris, a ceramic process engineer with experience in advanced flow components, states, “A nozzle succeeds when its geometry, material, and operating conditions are evaluated as one system.” This principle is easy to overlook. It also explains why identical-looking nozzles can perform very differently in production. Alumina, zirconia, silicon carbide, and other ceramics offer different balances of hardness, thermal stability, chemical resistance, and fracture sensitivity.
This guide examines which Ceramic Irregular Nozzle Manufacturer may offer the strongest combination of engineering skill, manufacturing control, and service reliability. It considers dimensional tolerance, surface finish, firing consistency, inspection records, and customization capability. Factory experience matters. So does communication.
A polished website is not proof.
The best manufacturers should explain their testing methods clearly. They should discuss nozzle drawings, operating temperature, pressure, media composition, and expected service life. However, no supplier can guarantee performance without complete application data. That is an important limitation, and buyers should acknowledge it.
Real evaluation may require sample testing, flow measurements, and field feedback. Small defects can appear only after repeated thermal cycling or continuous exposure to abrasive particles. Therefore, this comparison focuses on practical evidence rather than impressive claims. It aims to help engineers and purchasing teams make a careful, technically informed decision.
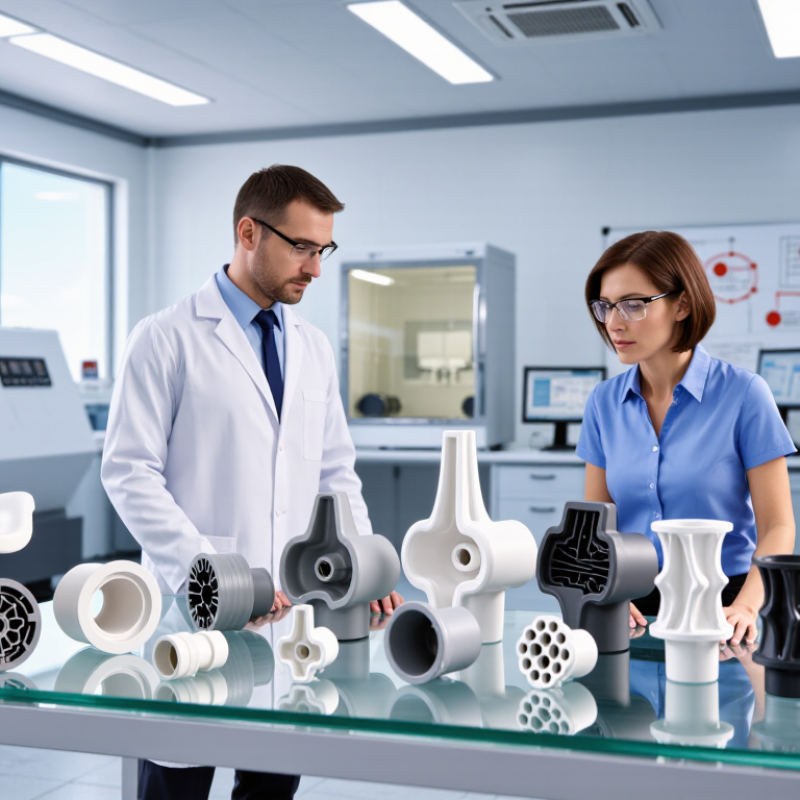
Table of Contents [Hide]
Definition and Industrial Role of Ceramic Irregular Nozzles
Which Is China’s Top Ceramic Irregular Nozzle Manufacturer?
Definition and Industrial Role of Ceramic Irregular Nozzles
A ceramic irregular nozzle is a precision component with a non-circular outlet or uneven internal channel. Its geometry directs gas, liquid, slurry, or abrasive particles toward a specific area. Unlike standard round nozzles, it can create wider coverage, a shaped spray pattern, or controlled impact. The design often uses technical ceramics because they resist heat, corrosion, wear, and chemical attack.
In industrial practice, these nozzles support thermal spraying, surface treatment, cleaning, coating, and material processing. A carefully shaped outlet can reduce dead zones inside a chamber. It may also improve material distribution across a curved or narrow workpiece. I have found that small dimensional changes can affect pressure loss and spray balance. That detail matters.
Very small errors matter.
When assessing a leading Chinese manufacturer, buyers should examine more than production capacity. Material purity, sintering control, dimensional inspection, and batch traceability are essential. Useful evidence includes tolerance reports, flow testing, thermal-shock testing, and service records from comparable applications. Engineers should also check whether the supplier can adjust the nozzle shape without weakening thin edges.
Ceramics are not unbreakable. Poor packaging, sudden temperature changes, or incorrect installation can cause failure. A reliable manufacturer should explain these risks clearly, rather than promise unlimited service life. Some specifications remain uncertain until testing begins. Pilot samples and measured operating data therefore provide stronger evidence than attractive catalog claims.