-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top Steel Grating Manufacturers and Suppliers
China’s steel industry supplies a wide range of Steel Grating for factories, platforms, walkways, drainage channels, stairs, and offshore facilities. However, choosing a manufacturer requires more than comparing prices. Buyers should examine material grades, bearing bar dimensions, welding quality, surface treatment, load capacity, and production consistency. A polished catalog cannot replace technical evidence.
According to steel grating specialist Michael R. Dawson, “A grating is only dependable when its design, welding, and installation details work together.” This practical view matters when evaluating China’s top Steel Grating manufacturers and suppliers. Experienced producers usually provide drawings, load tables, inspection records, and samples before large orders begin. They also understand the difference between welded grating, press-locked grating, riveted grating, and serrated surfaces. Small details matter. A smooth surface may look attractive, yet serrated bars can offer better traction in oily or wet areas.
This guide examines supplier capabilities from a buyer’s perspective. It considers factory experience, customization, quality control, certifications, packaging, communication, and export support. Some companies appear highly capable online but provide limited engineering information. That weakness deserves attention. Product quality can also vary between batches, especially when specifications remain vague. Therefore, buyers should request measurable standards instead of relying on broad claims. Site conditions, span length, pedestrian traffic, corrosion exposure, and maintenance expectations must shape the final choice. No supplier is perfect. Careful verification remains necessary, even when the first impression seems convincing.
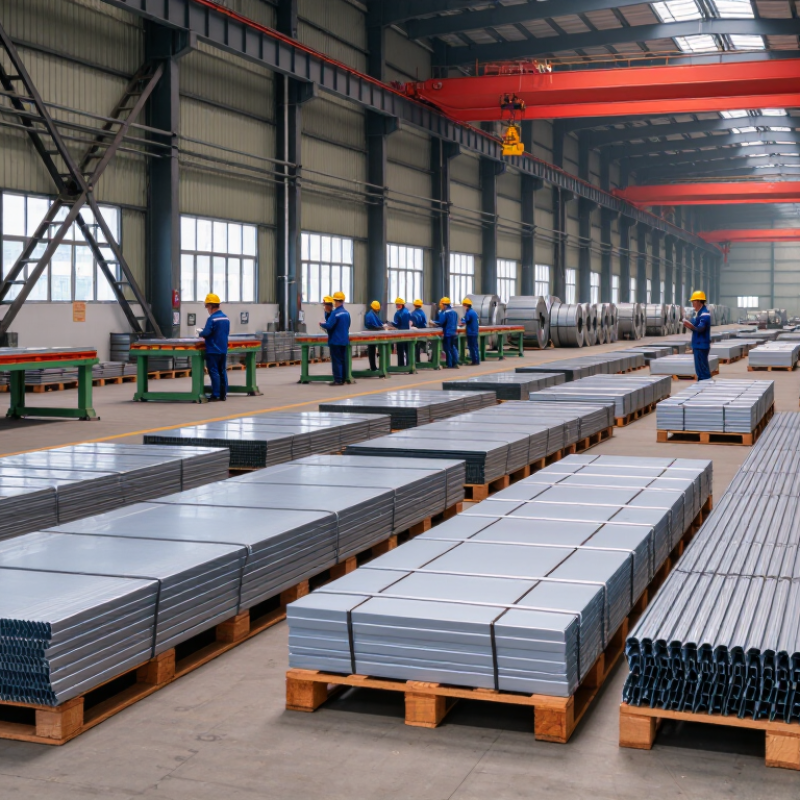
Table of Contents [Hide]
China’s Steel Grating Industry: Types, Features, and Market Scope
China’s steel grating industry serves construction, energy, transport, drainage, and industrial maintenance projects. Its main products include welded, press-locked, swage-locked, and riveted grating. Plain surfaces suit general walkways, while serrated surfaces improve grip in wet or oily areas. Steel, aluminum, and stainless steel offer different balances of strength, weight, and corrosion resistance. Galvanized steel remains widely selected because its zinc coating helps protect exposed surfaces.
Market scope continues to grow through infrastructure upgrades, factory expansion, and platform renovation. Buyers usually compare load capacity, bearing bar size, panel dimensions, surface treatment, and installation requirements. Reliable manufacturers and suppliers should provide drawings, material details, tolerance data, and traceable inspection records. Small details matter. A panel that fits poorly may create unsafe gaps or costly site adjustments. In my assessment, many purchasing mistakes begin with unclear application conditions, not production failure. Even experienced teams can overlook drainage, access frequency, or local weather exposure.
Tips: Confirm the design load before requesting quotations. Ask for coating thickness and test documentation. Check whether serrated edges are needed for the working environment. Request a sample when appearance and fit are critical. Do not judge suppliers by price alone; production consistency, communication, and after-sales responsiveness also influence total project value. Specifications can still be imperfect, so review them with the installer before approval.