-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Best Galvanized Steel Coil Manufacturer in China?
Choosing the best Galvanized Steel Coil Manufacturer in China requires more than comparing prices or browsing polished websites. A reliable decision begins with measurable production evidence. Buyers should examine steel grade, zinc coating mass, coil width, thickness tolerance, surface finish, and packing quality. These details affect performance long after the shipment leaves the factory.
Dr. Frank Goodwin, a recognized zinc-industry specialist, has explained: “Zinc protects steel through barrier protection and sacrificial, cathodic protection.” This principle matters in construction, automotive components, roofing, appliances, and industrial fabrication. A capable Galvanized Steel Coil Manufacturer should understand both protection mechanisms and their practical limits.
Look closely at the mill.
A serious producer can provide material certificates, coating test results, inspection records, and traceable production numbers. It should also discuss ASTM, EN, JIS, or GB requirements clearly. Vague promises are not technical evidence. Ask how the factory controls bath temperature, zinc composition, strip tension, cooling, and recoiling. Small process variations can create uneven coating, edge damage, or surface marks.
Experience matters, but it is not enough. A large factory may still respond slowly or handle complaints poorly. A smaller manufacturer may offer better communication and flexible production. This comparison can be uncomfortable.
No supplier is perfect.
Therefore, this guide evaluates Chinese manufacturers through quality control, production capacity, export experience, customization ability, delivery reliability, and after-sales support. It also considers an often-neglected issue: whether the supplier’s documents match the actual coils. Samples, factory audits, and independent inspections remain useful. A confident conclusion should be based on evidence, not attractive claims.
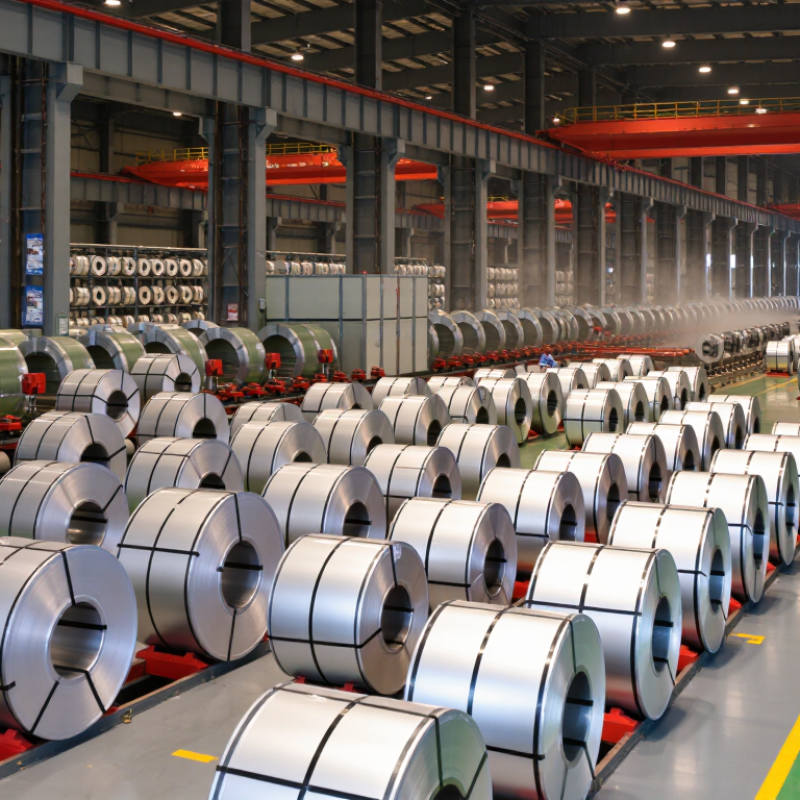
Table of Contents [Hide]
What Is Galvanized Steel Coil?
Galvanized steel coil is carbon steel protected by a zinc coating. Most coils use a hot-dip process, where cleaned steel passes through molten zinc. The zinc bonds closely with the surface and creates sacrificial protection. When moisture reaches exposed steel, zinc corrodes first. This delays rust and extends service life. Galvanized coil can be slit, roll-formed, painted, or pressed into roofing panels, ducts, automotive parts, and structural components. Coating mass, steel grade, thickness, and surface finish affect its performance.
When evaluating a manufacturer, request coating test results, dimensional tolerances, and batch traceability. Practical inspection may include a micrometer check, coating-gauge reading, bend test, and visual review. A bright surface can look excellent but still hide uneven coating. That assumption is not always correct. Storage also matters. Keep coils dry, raised from the floor, and separated with spacers. Trapped moisture can create white rust before installation.
Tips: Match the zinc coating to the environment. Coastal and humid areas usually need stronger protection. Confirm applicable standards before ordering. Ask for a sample and inspect the edges, where defects may appear first. Do not choose only by the lowest price. A cheaper coil may have thinner coating or inconsistent dimensions. The mistake is easy to make.