-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

7 Best Shot Blasting Equipment for Global Buyers
Choosing the right Shot Blasting Equipment is no longer a simple price comparison. Global buyers must examine cleaning capacity, abrasive recovery, dust control, automation, maintenance access, and energy use. A machine may look powerful on a showroom floor. Its real value appears beside a dusty conveyor, after months of production.
Recent market studies from Grand View Research and MarketsandMarkets indicate steady growth in industrial blasting and surface-treatment equipment. Their findings connect this growth with automotive production, fabricated steel, foundries, shipbuilding, and infrastructure renewal. Demand is increasing for enclosed systems, recyclable abrasives, and more consistent surface profiles. Exact market estimates differ between reports. That difference deserves attention, not dismissal.
As abrasive-blasting specialist Dr. David A. Summers has stated, “Surface preparation is a process, not a single operation.” This principle remains practical. Wheel speed, abrasive size, part geometry, and exposure time must work together. One setting rarely suits every component.
The seven machines reviewed here are not ranked by marketing language alone. They are assessed through working width, throughput, blast-wheel design, media efficiency, operator safety, service support, and documented results. Buyers should also request test samples, noise data, spare-parts lead times, and references from similar factories. Small details matter.
A cheaper machine can become expensive. Fast.
This guide has one limitation: supplier specifications are not always measured under identical conditions. Readers should verify performance independently before purchasing. The best Shot Blasting Equipment is the system that delivers repeatable preparation, controlled operating costs, and reliable results in the buyer’s actual production environment.
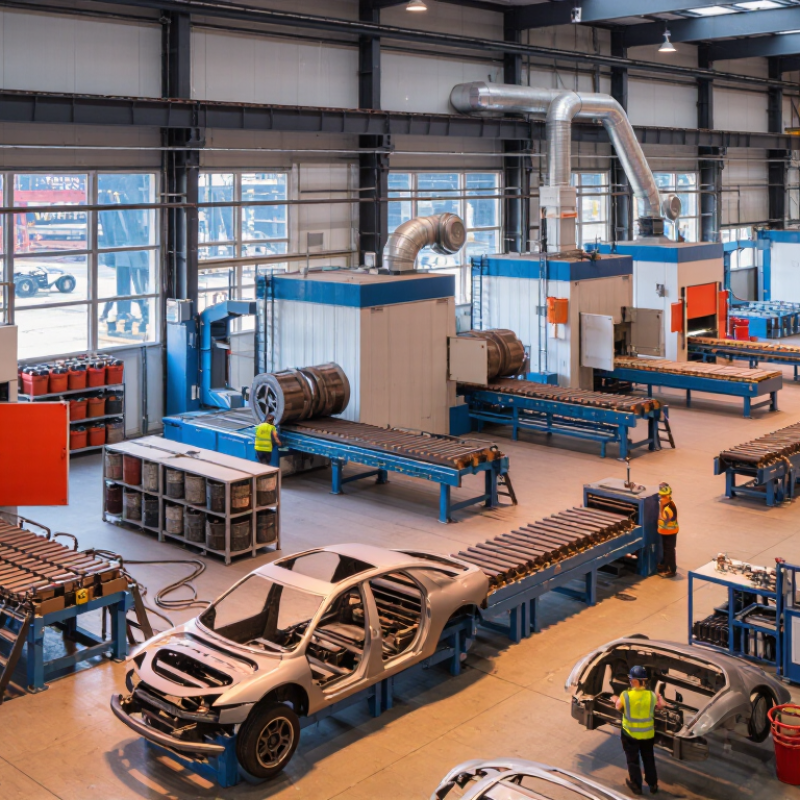
Table of Contents [Hide]
Shot Blasting Taxonomy: Seven Types, 0.3–2.5 mm Media, 25–500 kg Loads
7 Best Shot Blasting Equipment for Global Buyers
Shot blasting equipment is easier to compare when classified by work handling and load size. Seven common types include pressure-blast cabinets, suction-blast cabinets, tumble-belt machines, rotary-table machines, hanger systems, mesh-belt systems, and roller-conveyor machines. Each design suits a different production rhythm. Cabinets handle smaller batches, often around 25–80 kg. Rotary tables support repeated processing of castings with stable positioning. Hanger systems leave fewer contact marks on complex parts. Tumble-belt machines move many small components together, but fragile edges need careful testing.
Media selection strongly affects the result. Steel shot between 0.3 and 0.6 mm can clean smaller castings and remove light scale. Sizes from 0.8 to 1.5 mm offer stronger impact for general-duty work. Media from 1.8 to 2.5 mm suits heavy castings, thick scale, and aggressive preparation. Larger media can damage thin ribs. That mistake is expensive. Load capacity may range from 25 kg in compact cabinets to 500 kg in heavy conveyor or hanger systems. Actual capacity depends on part shape, not weight alone. A 200 kg load of tangled parts may block circulation. I have seen clean-looking surfaces fail later because hidden pockets received little impact. Trial runs should check coverage, media flow, dust control, and cycle time before purchase. Yet even these checks can miss one issue: operator loading habits often change the final finish.