-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

2026 How to Choose a Fusion Pipe Welder for Global Projects
Global infrastructure is expanding, but project conditions remain uneven. Remote sites, changing pipe standards, and limited technical support challenge welding teams daily.
The International Energy Agency’s World Energy Investment 2024 report estimates global energy investment will exceed 3 trillion dollars. Much of that spending supports grids, pipelines, utilities, and industrial facilities. The World Bank also reports continuing infrastructure gaps across emerging markets. These trends create demand for reliable joining equipment, including the Fusion Pipe Welder.
Selection requires more than comparing heating plates or clamp sizes. A suitable machine must match pipe material, diameter range, wall thickness, voltage conditions, and site temperatures. Data logging matters when contractors must prove joint consistency across borders. Calibration records matter too. Small details can decide whether a weld passes inspection.
Welding engineer John C. Villafuerte offers a useful principle: “Control the variables, and the joint will tell the truth.” His observation fits global projects well. Operators need clear procedures, repeatable pressure control, accurate temperature readings, and accessible spare parts.
The 2024 Global Welding Equipment Market report from Research and Markets identifies automation, infrastructure renewal, and energy projects as major growth drivers. Yet market forecasts cannot replace field judgment. A powerful welder may still fail in dusty conditions or unstable power.
That is the uncomfortable part. No machine is perfect. Buyers should test equipment with actual pipe samples, not only brochure specifications. This guide examines capacity, portability, standards support, operator training, service coverage, and total ownership cost. The right Fusion Pipe Welder should perform reliably beside the trench, not merely inside a showroom.
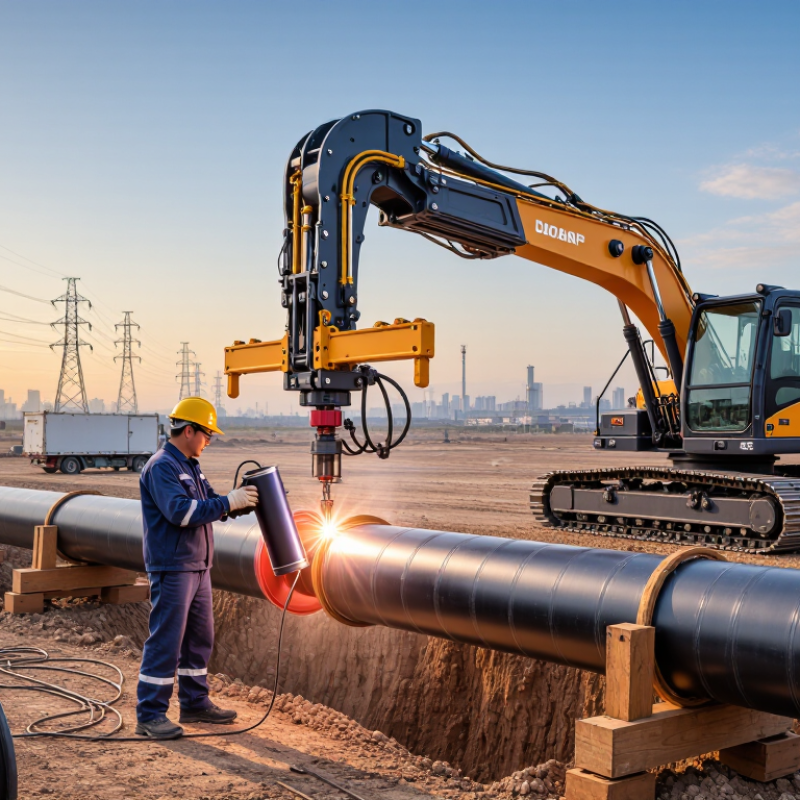
Table of Contents [Hide]
Define Project Scope: PE Grades, 40–1600 mm Sizes, Pressure, and Site Conditions
Choosing a fusion pipe welder starts with project scope, not machine appearance. Define the PE grade, SDR, diameter, pressure, and installation environment. Common polyethylene grades include PE80 and PE100, while diameters may range from 40 to 1,600 mm. ISO 4427 uses material strength, wall thickness, and safety coefficients to determine pressure capacity. For example, PE100 pipe with SDR11 has a theoretical working pressure near 16 bar at 20°C, before temperature and service adjustments. Confirm the actual rating with the pipe manufacturer’s technical data.
Machine capacity must match the largest joint. A 1,600 mm project needs high clamping force, stable hydraulic control, and accurate facing. Smaller 40 mm work may require different inserts or compact tooling. ISO 21307 and ASTM F2620 define controlled butt-fusion procedures, including heating, alignment, pressure, and cooling stages. PPI’s Handbook of Polyethylene Pipe also stresses clean surfaces, proper bead formation, and temperature control. These details matter in trenches, beside roads, and on exposed coastal sites.
Tips: Check wind, rain, dust, power supply, lifting access, and operator skill before selection. Use a data logger when quality records are required. For cold conditions, extend cooling time only under an approved procedure. I would not assume one machine fits every diameter. That assumption often fails. Pressure tables can also mislead when operating temperatures exceed 20°C. Review the project’s real fluid temperature, pressure surges, alignment tolerance, and emergency repair plan before ordering.