-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

2026 Top Carbon Steel Pipe Manufacturer Guide
Choosing a Carbon Steel Pipe Manufacturer in 2026 requires more than comparing price lists. Buyers need evidence of stable production, traceable materials, and dependable technical support. A polished website proves very little.
W. Edwards Deming, a renowned manufacturing quality expert, said, “Quality comes not from inspection, but from the improvement of the production process.” This principle remains highly relevant to carbon steel pipe production. A capable manufacturer controls chemistry at the melt stage, forming temperature, welding parameters, and final dimensional checks. Each batch should connect to a heat number, inspection report, and clearly stated standard.
Look closely at practical details. Can the supplier provide mill test certificates quickly? Are wall thickness and outside diameter checked with calibrated instruments? Does the factory explain hydrostatic testing without vague promises? These answers reveal experience.
A serious Carbon Steel Pipe Manufacturer should understand service conditions, not only product codes. Oil, water, structural, and low-temperature applications may require different grades, schedules, coatings, and testing routines. A pipe that looks perfect under warehouse lights can still fail after repeated pressure cycles or poor storage.
This guide examines leading manufacturers through production capability, certification, export experience, delivery performance, and customer feedback. It also considers weaknesses, because no supplier is ideal. Some companies offer broad catalogs but limited customization. Others provide excellent engineering but slower delivery.
The right choice is rarely the cheapest quote. It is the supplier that can prove consistency, communicate clearly, and accept technical scrutiny. One overlooked document can become an expensive project delay.
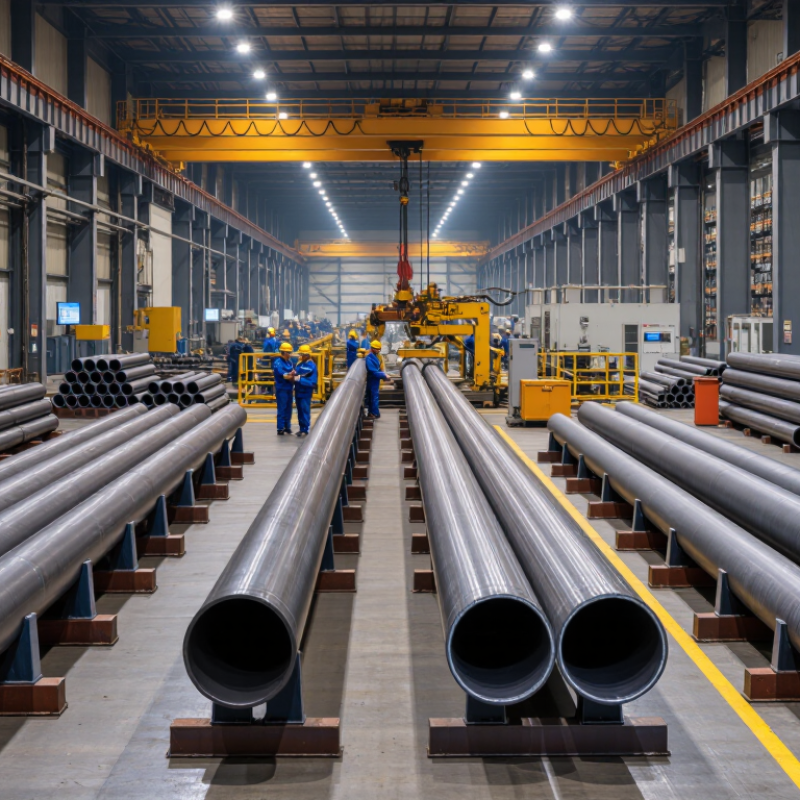
Table of Contents [Hide]
Carbon Steel Pipe Fundamentals: NPS 1/8–48, Schedules, and Grades
Carbon steel pipe sizing begins with NPS, or Nominal Pipe Size, from 1/8 through 48. NPS is not the exact outside diameter, especially below NPS 12. For example, NPS 2 pipe has an outside diameter near 2.375 inches. Larger sizes follow different dimensional conventions. This detail matters when checking fittings, supports, and welding alignment.
The schedule identifies wall thickness, not a direct pressure rating. Common schedules include 5, 10, 40, 80, 120, 160, and XXS, but availability changes with pipe size. NPS 2 Schedule 40 and NPS 2 Schedule 80 share the same outside diameter. Their internal diameters differ because the walls are thicker. Actual dimensions should be verified against ASME B36.10M tables before ordering. A schedule number alone cannot replace engineering calculations.
Grade selection connects the pipe to its service. ASTM A53 is widely used for general mechanical and pressure applications, while ASTM A106 is commonly selected for seamless high-temperature service. Other grades may suit low-temperature impact requirements or heavier structural duty. Check chemical composition, yield strength, tensile strength, weldability, and test requirements. Field inspections often find that coating damage, oval ends, or incorrect wall thickness causes more trouble than the grade itself. That is easy to overlook. Corrosion allowance, operating temperature, fluid chemistry, and joining method should be reviewed together. Mistakes happen when one attractive specification controls the entire purchase.