-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

2026 Best Boiler Centrifugal Fan for Global Buyers
Choosing the 2026 Best Boiler Centrifugal Fan requires more than comparing catalog prices. Global buyers need reliable airflow, stable pressure, efficient motors, and documented testing. A suitable Boiler Centrifugal Fan must match the boiler’s fuel type, furnace size, flue resistance, and operating temperature. Small mismatches can cause noisy operation, unstable combustion, or unnecessary energy loss.
Dr. David A. Tillman, a recognized combustion-systems specialist, states, “Combustion equipment performs only as well as its air system.” This principle remains practical for modern boiler projects. Buyers should examine fan curves at the actual duty point, not only the maximum airflow figure. They should also check impeller balance, housing steel grade, bearing protection, vibration limits, and motor efficiency. Site experience matters. Dust, moisture, corrosive gases, and frequent load changes can quickly expose weak design choices.
No universal best fan exists. That is the uncomfortable truth. A compact fan may suit a clean industrial plant but fail in a biomass boiler room. A premium model may offer excellent efficiency yet create maintenance difficulties in remote locations. This guide compares leading options for 2026 through performance data, service access, noise control, customization, spare-parts availability, and supplier credibility. Product certificates and test reports deserve careful review. So do installation drawings.
Some specifications remain unclear.
Responsible buyers should request operating guarantees, inspection records, warranty terms, and realistic delivery schedules. The strongest choice balances engineering performance with long-term ownership cost. It should work reliably on ordinary production days, not only in ideal factory tests.
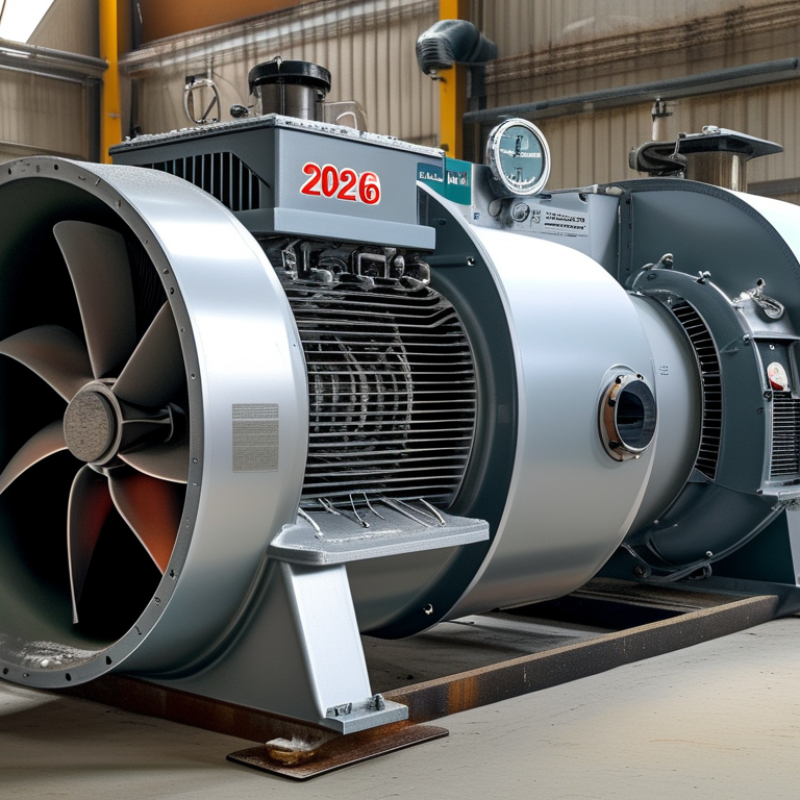
Table of Contents [Hide]
What Is a Boiler Centrifugal Fan and How Does It Work?
What Is a Boiler Centrifugal Fan and How Does It Work?
A boiler centrifugal fan moves air or flue gas through a combustion system. Its rotating impeller draws gas into the center and pushes it outward through curved blades. The fan housing then directs this flow toward the outlet. This design creates the pressure needed to overcome burners, ducts, heat exchangers, filters, and dampers.
In field inspections, technicians usually check the motor, bearings, impeller, housing, and flexible connections. A forced-draft fan sends fresh air into the furnace. An induced-draft fan pulls combustion gases toward the stack. Both functions help control combustion and furnace pressure. Speed controllers or dampers adjust the airflow as boiler demand changes. Selection should match airflow, static pressure, gas temperature, dust level, altitude, and operating hours. A fan that is too small may reduce combustion efficiency. An oversized unit can waste power and create unstable pressure.
Watch the details.
During commissioning, operators should compare actual airflow with design values. They should also record vibration, motor current, bearing temperature, and unusual noise. A quiet fan is not always a healthy fan. Hidden imbalance can develop before sound changes. In my experience, installation alignment is often underestimated. Even a well-designed fan may perform poorly when ducts are sharply bent or supports are loose. Regular cleaning matters too, because dust buildup can disturb impeller balance and increase energy use. Careful measurements remain more reliable than appearance alone.